Manufacturing
November 17 2026
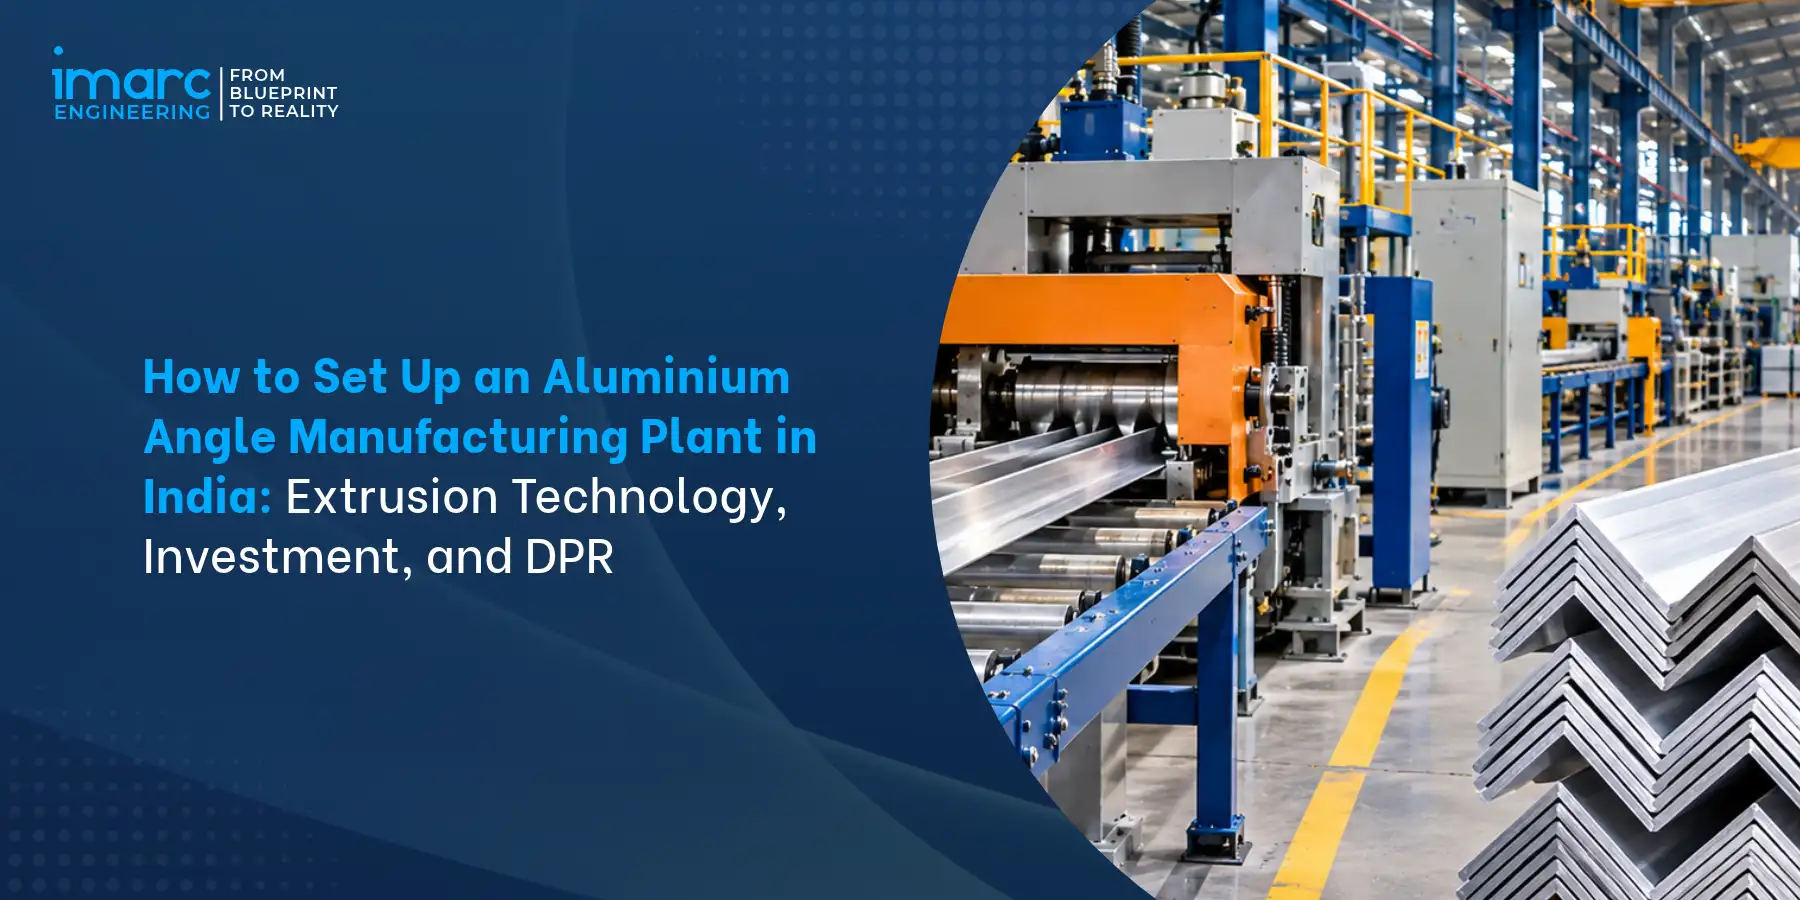
How to Set Up an Aluminium Angle Manufacturing Plant in India: Extrusion Technology, Investment, and DPR (2026)
Introduction
An aluminium angle manufacturing plant in India presents an opportunity for investors, project developers and extrusion manufacturers to serve demand from the construction, infrastructure and industrial fabrication sectors. The country's established aluminium billet supply base and potential for import substitution further support the sector's growth prospects.
However, project viability depends on more than market demand. Key factors such as extrusion yield, die life, press utilisation and billet procurement costs directly influence production efficiency, operating margins and overall project economics. These considerations must be evaluated during the planning and feasibility assessment stages.
A poorly planned plant fails predictably. An undersized press forces expensive die redesign. A badly laid-out runout table inflates scrap. A missing ageing furnace blocks 6061-T6 supply. A plant built for multiproduct work but costed as a dedicated angle line misstates both CAPEX and breakeven.
Scope of this Guide
This guide answers one question: how can investors establish an aluminium angle manufacturing plant in India, select appropriate extrusion technology, estimate investment requirements and prepare a DPR to evaluate project feasibility? It covers billet-based direct extrusion only. Primary smelting, casting-house operations and general fabrication are excluded. It addresses product and alloy planning, raw materials, process steps, finishing and testing, machinery, utilities, approvals, and capital and operating cost composition for dedicated and multiproduct configurations.
Table of Contents
- Introduction
- Why Aluminium Angle Manufacturing Plant in India Matters for Investors in 2026
- What an Aluminium Angle Manufacturing Plant in India Is and Why It Matters
- Aluminium Angle Manufacturing Plant in India: Product Types, Alloys and Capacity Planning
- Raw Materials and Consumables for an Aluminium Angle Manufacturing Plant in India
- Aluminium Angle Manufacturing Plant in India: Extrusion Process Steps from Billet to Runout
- Aluminium Angle Manufacturing Plant in India: Finishing, Quality Testing and DPR Inputs
- Machinery, Layout and Utilities for an Aluminium Angle Manufacturing Plant in India
- Environmental Compliance, Approvals and Project Economics for an Aluminium Angle Manufacturing Plant in India
- Detailed Project Report (DPR) for an Aluminium Angle Manufacturing Plant
- Conclusion
1. Why Aluminium Angle Manufacturing Plant in India Matters for Investors in 2026
Four conditions make an aluminium angle manufacturing plant in India worth structured evaluation.
1.1 Construction, Fabrication and Industrial Demand
Aluminium angles serve window and door frames, curtain-wall brackets, solar mounting structures, transport body framing, electrical enclosures, shelving and general fabrication. Demand follows construction, infrastructure, renewable-energy installation and industrial fabrication cycles. Angles are a commodity-grade section, so buyers are fabricators and dealers who purchase on price, tolerance consistency and stock availability. A plant should map its target customers and delivery radius before sizing the press.
1.2 Domestic Billet Supply and Import Substitution
India has integrated primary producers and several secondary billet casters supplying extrusion-grade 6063 and 6061 billets. Domestic billet availability reduces import exposure for the aluminium extrusion plant in India, while imported extrusions remain a competitive pressure on commodity profiles. Local plants win on lead time, custom lengths and tolerance responsiveness. Billet contracts, pricing formulas and supplier concentration must be tested during feasibility.
1.3 Policy and Investment Ecosystem
Investors should verify state industrial policies for capital subsidy, power tariff concessions and SGST-linked incentives, along with MSME classification benefits for smaller configurations. Eligibility depends on investment quantum, location category and sector listing. Incentive net present value, not face value, should enter the financial model, and conditions on employment or production milestones should be read from the actual notification (Figures are indicative in nature, may vary).
1.4 Cost of Poor Planning
Typical errors include selecting an oversized press for thin-wall angles, ignoring die inventory cost, under-sizing the cooling and puller sections, omitting a stretcher and ageing capacity for heat-treatable alloys, and treating a dedicated angle line as interchangeable with a multiproduct plant. Each error raises scrap, lowers yield and extends payback. Disciplined engineering up front prevents them.
2. What an Aluminium Angle Manufacturing Plant in India Is and Why It Matters
Definition and scale logic determine every downstream engineering decision.
2.1 Definition and Process Boundary
An aluminium angle manufacturing plant converts cast aluminium billets into L-section profiles by hot direct extrusion. A heated billet is pushed through a steel die in a hydraulic press, cooled on a runout table, stretched, cut, aged where required and packed. It differs from primary aluminium smelting (electrolysis of alumina) and from fabrication shops that cut and weld bought-in sections.
2.2 Dedicated Angle Plant versus Multiproduct Extrusion Plant
A dedicated aluminium angle production line runs a narrow die family, equal and unequal angles of limited leg sizes, so it uses one press range, standard handling and high utilization. A multiproduct aluminium profile manufacturing plant runs hollow, architectural and industrial sections, needs larger die stores, tighter surface standards, more frequent changeovers and usually anodising or powder coating. Dedicated lines carry lower CAPEX and simpler operations but depend on one product's margin.
2.3 Scale Determinants
Scale follows press tonnage, billet diameter, product mix, shifts and finishing scope. Small plants use 600 to 900 ton presses with 5 to 7 inch billets; mid-size plants use 1,200 to 1,800 ton presses with 7 to 9 inch billets; larger multiproduct plants use 2,000 ton and above. Output is indicative at roughly 2,000 to 4,000 tonnes per year per small press and 6,000 to 12,000 tonnes per year for a mid-size press, depending on yield and utilization (Figures are indicative in nature, may vary).
2.4 Plant Sections
| Section | Function | Key Equipment |
|---|---|---|
| Billet Storage | Receive and stage billets | Racks, EOT crane 5-10 t |
| Billet Heating | Heat billets to 430-500 C | Gas or induction furnace |
| Die Shop | Preheat and maintain dies | Die oven 450-480 C |
| Extrusion Press | Form angle profile | 600-2,000 ton hydraulic press |
| Cooling and Runout | Quench and convey profile | Air or water quench, 30-45 m table |
| Stretching and Cutting | Straighten, cut to length | Stretcher 40-100 t, saw |
| Ageing Section | Age 6061 to T5/T6 | Ageing furnace 160-200 C |
| Finishing (Optional) | Anodise or powder coat | Tanks, coating line |
| Utilities | Power, air, cooling water | Transformer, compressor, cooling tower |
| Effluent Treatment | Treat finishing wastewater | pH, neutralization, filter press |
3. Aluminium Angle Manufacturing Plant in India: Product Types, Alloys and Capacity Planning
Product definition fixes press, die and finishing decisions before any machine is quoted.
3.1 Equal and Unequal Aluminium Angles
Equal angles have identical legs, for example 25 x 25 x 3 mm to 100 x 100 x 10 mm. Unequal angles carry different legs, for example 50 x 25 x 3 mm. Thickness commonly ranges from 1.5 to 12 mm. Die cost and extrusion ratio differ by size, so a catalogue of 40 to 80 sections is typical for a dedicated line. Sharp inside corners need controlled radii to protect die life.
3.2 Alloy Grades and Tempers
6063 in T5 or T6 is the dominant grade for general angles, offering good extrudability and surface. 6061 in T6 serves structural and higher-strength needs and requires ageing capacity. Alloy 6082 appears in some structural applications. Alloy and temper selection drives billet specification, quench intensity, stretching and ageing furnace sizing.
Product specifications should be verified against applicable Indian Standards, including relevant requirements for chemical composition, mechanical properties, dimensional tolerances and testing methods. The applicability of IS 733 and IS 1285 should be confirmed for the selected aluminium angle products.
3.3 Capacity and Product-Mix Planning
Capacity planning starts from press tonnage and extrusion ratio. A mid-size press running 6063 angles at moderate ratios typically achieves 40 to 80 kg per minute of extrudate depending on section, with practical utilization of 65 to 80 percent over two to three shifts. Product mix by leg size sets average yield, die changeover frequency and billet length strategy (Figures are indicative in nature, may vary).
3.4 Location and Cluster Selection
Extrusion clusters exist in Gujarat, Maharashtra, Tamil Nadu, Telangana and the northern industrial belt. Site selection weighs billet supplier distance, three-phase HT power reliability, gas or LPG availability, customer proximity, water for cooling and effluent disposal if finishing is planned. Press foundations need competent bearing strata, so geotechnical data is a gateway item.
4. Raw Materials and Consumables for an Aluminium Angle Manufacturing Plant in India
Billet quality and consumables decide yield, surface and die life.
4.1 Aluminium Billets and Alloy Chemistry
Extrusion billets are homogenized, cast 6063 or 6061 logs in diameters of 5, 6, 7, 8 and 9 inches and lengths of 5 to 7 metres, sawn to press length. 6063 chemistry centres on 0.45 to 0.9 percent magnesium and 0.2 to 0.6 percent silicon. Homogenization of billets controls Mg2Si precipitates and extrudability. Suppliers should provide mill certificates, grain-size and surface-defect limits.
4.2 Extrusion Dies and Tooling
Dies are H13 hot-work tool steel, nitrided after machining for wear resistance, with bolsters, backers, rings and die holders sized to the press. Angle dies are single-hole or multi-hole flat dies, with bearing lengths adjusted to balance flow. Die life depends on alloy, ratio and nitriding quality. A starting die inventory for a dedicated line represents a significant working-capital line.
4.3 Finishing and Packaging Consumables
Where surface finishing is planned, consumables include caustic soda, sulphuric acid, nickel acetate sealing salts and dyes for anodising, or polyester powder and pretreatment chemicals for powder coating. All lines need packing consumables: interleaving paper, stretch film, PE sleeves, wooden dunnage and strapping. Gas for billet furnaces and ageing, and nitrogen or inert gas where specified, form the main fuel consumables.
4.4 Storage and Safety
Billets are stored in racks with clean, dry bases to avoid moisture ingress, which is a steam-explosion hazard on hot billets and in the die oven. Chemicals for finishing need segregated acid and alkali storage with secondary containment, eyewash stations and ventilation. Scrap segregation by alloy preserves remelt value.
5. Aluminium Angle Manufacturing Plant in India: Extrusion Process Steps from Billet to Runout
The aluminium angle extrusion process runs as a controlled hot-working sequence where temperature and speed windows decide quality.
5.1 Billet Heating
Billets are heated in a gas-fired or induction furnace to about 430 to 500 degrees C for 6063, with taper or gradient heating to counter the cooling effect at the press container. Log furnaces heat full-length billets; hot-log shears cut to length. Temperature uniformity within plus or minus 10 degrees C is typically targeted. Cold or uneven billets raise press load and cause surface tearing.
5.2 Die Preparation and Preheating
Dies are inspected, nitrided if needed, and preheated in a die oven at 450 to 480 degrees C for several hours before loading. The container is held near 400 to 450 degrees C. Correct die preheat reduces thermal shock and surface defects. Die correction, polishing and bearing adjustment happen in the die shop between runs.
5.3 Extrusion
The hydraulic press pushes the billet through the die at ram speeds that deliver exit speeds of a few metres to over 30 metres per minute depending on section and alloy. A butt shear removes the discard, and a hot saw or puller handles the leading end. Extrusion ratio, defined as billet cross-section divided by profile cross-section, commonly falls between 20 and 60 for angles, balancing press load and dimensional control.
5.4 Cooling, Runout and Puller
Profiles exit onto a runout table and are tracked by a puller that maintains tension and prevents distortion. Quenching with forced air, fog or water spray achieves T5 cooling rates; 6061-T6 needs faster water quench to hold solute. Typical runout length is 30 to 45 metres. Cooling rate control determines mechanical properties and residual stress, which in turn affect straightness.
6. Aluminium Angle Manufacturing Plant in India: Finishing, Quality Testing and DPR Inputs
Downstream operations convert hot extrudate into specification-grade product and generate the data a DPR needs.
6.1 Stretching, Straightening and Cutting
Cooled profiles move to a stretcher where 0.5 to 3 percent permanent elongation removes twist and bow and relieves residual stress. Stretcher capacity of 40 to 100 tonnes suits angle sections. Stretched lengths are sawn to order lengths, often 3 to 6 metres, by a double-head circular saw after discarding gripped ends. Extrusion yield is typically 80 to 90 percent depending on mix (Figures are indicative in nature, may vary).
6.2 Ageing Furnace
Artificial ageing at about 160 to 200 degrees C for 2 to 8 hours develops T5 or T6 temper. Batch ageing ovens with forced circulation hold plus or minus 5 degrees C. Furnace loading and basket design affect uniformity. Hardness checks by Webster or Brinell methods, and tensile testing on representative lengths, confirm temper against grade requirements.
6.3 Optional Surface Finishing
A dedicated angle plant may supply mill finish only. Where anodising or powder coating is added, the line requires degreasing, etching, desmutting, anodic oxidation at roughly 15 to 25 micron thickness, sealing, or chromate-free pretreatment and powder cure at about 180 to 200 degrees C. Finishing adds CAPEX, effluent handling and compliance obligations, so it is a deliberate scope decision.
6.4 Inspection, Standards and DPR Inputs
Inspection covers dimensional checks using vernier calipers and profile projectors against applicable product specifications, along with straightness, twist, angle squareness, surface defects, spectrometer-based chemistry verification and mechanical testing. Records feed the DPR technical section: yield, scrap, rework, die consumption and energy per ton. These plant parameters convert directly into OPEX assumptions.
7. Machinery, Layout and Utilities for an Aluminium Angle Manufacturing Plant in India
Machinery, building, and utilities must be specified together because press foundations and crane heights lock the civil design.
7.1 Extrusion Press and Billet Equipment
The core is a front-loading direct hydraulic extrusion press, with oil-hydraulic or direct-drive pump systems. Press selection weighs billet diameter, specific pressure, container size, speed and dimensional capability. For angles, a 1,000 to 2,000 ton press is common. Billet equipment includes log furnace, hot-log shear, billet loader and butt shear. Press foundations are heavily reinforced and isolated, and need a deep pit for hydraulic and tooling systems.
7.2 Runout, Puller, Stretcher and Saw
The runout table carries cooling fans or water sprays, a double puller for continuous extrusion, a transfer table, a stretcher with gripping jaws and a finish saw with measuring stops. Handling tables and ageing baskets complete the line. Cooling system capacity must match the section mass and speed.
7.3 Utilities, Layout and Material Handling
A 1,200 to 1,800 ton line typically has a connected load of 1.5 to 3 MVA at 11 kV or 33 kV with a transformer and LT distribution. Cooling water circulates at 30 to 100 cubic metres per hour through a cooling tower. Compressed air at 6 to 8 bar serves pneumatics. Gas consumption for billet heating and ageing is significant. Layout runs billet store, furnace, press, runout, stretcher, saw, ageing, packing and dispatch in a straight flow. Bay width of 24 to 30 meters and crane headroom for EOT cranes of 10 to 20 tonnes are typical. A separate die shop sits close to the press (Figures are indicative in nature, may vary).
7.4 Key Machinery
Rows below show the main equipment categories.
| Category | Equipment | Primary function | Indicative selection basis |
|---|---|---|---|
| Extrusion | Hydraulic extrusion press | Forces heated aluminium billets through dies to produce angle profiles | Press tonnage and billet diameter |
| Billet heating | Gas-fired log furnace and hot shear | Heats billets and cuts them to the required extrusion length | Billet dimensions and heating capacity |
| Die management | Die oven and die shop equipment | Preheats, inspects and maintains extrusion dies | Die dimensions and production mix |
| Cooling and handling | Runout table, quenching system and puller | Cools extruded profiles and maintains controlled movement during extrusion | Profile dimensions and extrusion speed |
| Stretching | Hydraulic stretcher | Straightens profiles and reduces residual stress | Profile dimensions and stretching force |
| Cutting | Finish saw | Cuts extruded profiles to specified commercial lengths | Required product lengths |
| Ageing | Batch ageing furnace | Develops required mechanical properties and tempers | Alloy grade and heat-treatment requirements |
| Inspection | Spectrometer and tensile testing machine | Verifies chemical composition and mechanical properties | Applicable product specifications |
| Utilities | Transformer, compressor and cooling tower | Supplies electrical power, compressed air and process cooling | Equipment load and utility demand |
| Finishing (optional) | Anodising or powder coating line | Provides surface protection and decorative finishing | Customer requirements and product scope |
8. Environmental Compliance, Approvals and Project Economics for an Aluminium Angle Manufacturing Plant in India
Compliance and cost structure convert a technical design into a bankable investment case.
8.1 Effluent, Emissions and Waste
A mill-finish plant generates limited effluent: cooling blowdown, die cleaning caustic and occasional spills. Die cleaning in caustic soda baths produces alkaline sludge needing neutralization. Finishing lines add acidic and alkaline rinse water and aluminium hydroxide sludge, needing neutralization, clarification and filter-press dewatering. Furnace flue gases and oil mist from hydraulics need stack monitoring. Pollution limits follow State Pollution Control Board consent conditions.
8.2 Licences and Approvals
Key approvals may include company registration, Udyam registration for eligible MSMEs, State Pollution Control Board Consent to Establish and Consent to Operate under applicable environmental laws, factory registration, licensing and plan approvals under prevailing occupational safety and factory regulations, fire NOC, and electricity connection approvals.
Other requirements may include boiler or pressure vessel registration, where applicable, GST registration and EPF/ESI compliance based on statutory applicability. Product conformity and any mandatory BIS certification requirements should be verified against relevant Indian Standards and applicable Quality Control Orders.
The requirement for Environmental Clearance should be assessed against the EIA Notification, 2006, as amended, based on the proposed manufacturing activities and project configuration.
8.3 CAPEX and OPEX Composition
Capital expenditure for an aluminium angle manufacturing plant depends on press capacity, production configuration, automation and finishing requirements. Major CAPEX components include:
- Plant and Machinery: Extrusion press, billet heating furnace, die oven, runout table, stretcher, cutting equipment and ageing furnace.
- Civil and Structural Works: Factory building, reinforced press foundation, equipment foundations, storage areas and material handling infrastructure.
- Utilities: Electrical systems, transformers, cooling towers, compressors, gas supply and water circulation systems.
- Dies and Tooling: Extrusion dies, bolsters, die holders and associated tooling.
- Finishing and Environmental Systems: Anodising or powder coating equipment, effluent treatment and pollution control systems, where applicable.
- Pre-operative Expenses: Engineering, installation, commissioning, approvals and contingency.
Operating expenditure includes raw material procurement, energy, labour, die maintenance, consumables, repairs, packaging and administrative expenses. Billet procurement is a major raw material cost and should be accounted for separately from conversion costs. Conversion costs cover expenses associated with transforming billets into finished profiles, including energy, labour, tooling consumption, maintenance and production overheads.
The final cost structure should be developed using supplier quotations, production assumptions, expected material yield and actual operating requirements rather than generic percentage allocations.
8.4 Project Economics
Project economics should be evaluated using the selected production capacity, machinery specifications, site conditions, product mix and finishing scope. The total investment should be established through equipment vendor quotations, civil cost estimates, utility requirements, installation expenses and pre-operative costs.
Working capital requirements should account for billet inventory, work-in-progress, finished goods, die inventory, operating expenses and customer receivables, considering supplier credit and customer payment terms.
The financial model should evaluate raw material prices, billet procurement premiums, extrusion yield, production utilization, energy consumption, selling prices and operating costs. Key financial indicators include break-even production, cash flow, DSCR, IRR, NPV and payback period.
Investment estimates should distinguish between dedicated angle lines and multiproduct extrusion facilities, particularly where anodising or powder coating is included. Actual project costs should be finalised only after technical specifications, site requirements and vendor quotations are established.
9. Detailed Project Report (DPR) for an Aluminium Angle Manufacturing Plant
A Detailed Project Report (DPR) evaluates the technical feasibility, investment requirements and financial viability of an aluminium angle manufacturing plant. It consolidates market research, engineering specifications, machinery selection, infrastructure planning, regulatory requirements and financial projections into a structured implementation plan.
9.1 Technical Feasibility
The technical assessment should establish the product portfolio, alloy grades, temper requirements, production capacity and manufacturing configuration. It should evaluate extrusion press specifications, billet dimensions, machinery requirements, production yield, utilities, plant layout and quality control systems.
9.2 CAPEX and OPEX Assessment
The investment assessment should cover machinery procurement, civil construction, electrical infrastructure, utilities, dies and tooling, installation, commissioning and pre-operative expenses. Operating expenditure should include billet procurement, energy, labour, maintenance, consumables and administrative costs.
9.3 Working Capital Requirements
Working capital estimates should account for raw material inventory, work-in-progress, finished goods, operating expenses and receivables. Supplier credit periods, customer payment terms and inventory requirements should be incorporated into the assessment.
9.4 Financial Projections and Funding
Financial projections should include estimated revenue, production costs, operating margins, cash flows and profitability. Funding requirements should consider promoter contribution, term loans, working capital facilities and applicable financial incentives, subject to eligibility and lender requirements.
9.5 Implementation Schedule
The implementation plan should cover site finalization, engineering, statutory approvals, civil construction, machinery procurement, equipment installation, utility connections, trial production and commercial commissioning. Project milestones should be developed based on vendor delivery schedules and approval timelines.
9.6 Sensitivity and Risk Analysis
Sensitivity analysis should evaluate the impact of changes in billet prices, selling prices, extrusion yield, capacity utilization, energy costs and working capital requirements. Financial indicators such as DSCR, IRR, NPV and break-even should be assessed under different operating scenarios.
9.7 Plant Setup and DPR Checklist
Before proceeding with implementation, investors should verify the following:
- Market and Product Planning: Target customers, product dimensions, alloy grades, temper requirements and production capacity.
- Technical Feasibility: Extrusion press selection, billet specifications, machinery requirements, production process and quality standards.
- Site and Infrastructure: Land suitability, geotechnical assessment, plant layout, power availability, water supply, gas supply and material handling.
- Raw Materials: Billet sourcing, supplier quotations, die inventory, consumables and procurement arrangements.
- Regulatory Approvals: Applicable factory registration and licensing, pollution control consents, fire safety approvals, electricity connection approvals and other statutory permissions.
- Financial Planning: CAPEX, OPEX, working capital, funding structure, financial projections, and sensitivity analysis.
- Implementation: Engineering schedule, machinery procurement, construction, installation, trial runs and commercial commissioning.
A comprehensive DPR provides investors and lenders with a basis for evaluating project viability, funding requirements and implementation risks before committing capital.
Conclusion
An aluminium angle manufacturing plant in India succeeds when product definition, extrusion technology, utilities and compliance are planned as one integrated design rather than a machinery shopping list. The logic runs from the target angle catalogue and alloy to press tonnage and billet diameter, then to furnaces, runout, stretching, ageing and utilities, and finally to approvals, CAPEX, OPEX and the DPR financial model. Each stage constrains the next, so errors upstream surface as scrap, downtime or stranded capital.
Three priorities decide the outcome:
- First, fix product mix, alloy and tempers before selecting the press, and decide early whether the facility is a dedicated angle line or a multiproduct plant.
- Second, lock billet sourcing terms, yield assumptions and die strategy, because billet cost and die consumption drive margin more than any other variable.
- Third, run site, power, effluent and approval verification in parallel with engineering so that machinery orders match an approved layout.
Addressing these priorities early can reduce technical risks, improve project planning, and support more reliable investment decisions.
PURSUING AN ALUMINIUM ANGLE MANUFACTURING PLANT IN INDIA?
IMARC Engineering supports investors, extrusion manufacturers and project sponsors with capacity and feasibility planning, site selection, plant layout, extrusion press and furnace selection, utilities, effluent treatment, regulatory approvals, DPR preparation and capital investment planning. The advisory covers equal and unequal aluminium angles, including billet heating, extrusion, cooling, stretching, cutting, ageing and optional finishing, with project-specific infrastructure and commissioning planning.
→ Schedule an aluminium angle plant scoping consultation with an IMARC specialist
Frequently Asked Questions
Start by defining the product range, alloy grades and production requirements. Conduct a feasibility study, select a suitable site, plan the plant layout and utilities, obtain applicable approvals, procure machinery and complete installation, testing and commissioning.
The process involves billet storage, heating, die preparation, hot extrusion, cooling and quenching, stretching, cutting and ageing. Finished profiles undergo quality inspection before optional surface finishing, packing and dispatch.
Key machinery includes a hydraulic extrusion press, billet heating furnace, hot shear, die oven, runout table, quenching system, puller, stretcher, finish saw and ageing furnace. Supporting equipment includes material-handling systems, utilities and quality-testing instruments.
Investment depends on production capacity, machinery specifications, plant configuration, site development, utilities and finishing requirements. Major cost components include machinery, dies, civil works, electrical infrastructure, installation and pre-operative expenses. A project-specific assessment is needed to determine the investment.
Select the press based on the product dimensions, alloy grades, billet specifications, extrusion ratio and production requirements. Other considerations include press capacity, container size, operating speed, dimensional accuracy and compatibility with the planned die configuration.
The primary raw material is homogenised aluminium extrusion billet, generally sourced in suitable alloy grades. Other requirements include extrusion dies, heating fuel or electricity, packaging materials and consumables for optional surface-finishing operations.
An aluminium extrusion plant requires reliable high-tension power, reinforced equipment foundations, material-handling systems, cooling water, compressed air and fuel supply. It also needs suitable storage, a die maintenance area and effluent treatment facilities where surface finishing is undertaken.
Applicable requirements may include pollution control consents, factory approvals, fire clearance, electricity connection approvals and relevant business and labour registrations. Product specifications should be assessed against applicable Indian Standards, with BIS certification requirements verified for the proposed products.
A DPR should cover market demand, product specifications, technical feasibility, production capacity, machinery, plant layout, utilities, CAPEX, OPEX and working capital. It should also include financial projections, funding requirements, regulatory approvals, implementation planning and risk analysis.
Extrusion yield depends on billet quality, die condition, section geometry, process control and material losses during production. Profitability is influenced by billet procurement costs, selling prices, press utilisation, energy consumption, tooling expenses, maintenance and product quality.
Recent Post
Trusted by Industry Leaders
We partner with global enterprises and ambitious businesses across sectors to deliver operational excellence, strategic insights, and sustainable growth through integrated solutions.
Success in Their Words
Real feedback from clients across industries. Discover how our solutions delivered measurable impact and operational excellence.
I wanted to express my sincere appreciation for your efforts in handling this matter. Your dedication and commitment have been truly commendable, and it is evident that you have put in tremendous hard work and expertise into resolving the issues at hand. We are greatly interested in continuing our collaboration with you in the future, as your professionalism and reliability have made you a trusted partner. Thank you once again for your invaluable contribution. We look forward to strengthening our partnership ahead.
It has been a pleasure working with the IMARC team. The insights provided were structured, clear, and highly valuable, helping us strengthen both our technical and financial planning with confidence. We deeply appreciate the team’s professionalism, responsiveness, and attention to detail throughout the engagement. Every requirement was well understood and effectively incorporated, resulting in a comprehensive and actionable output. Overall, our experience has been excellent, and I would gladly recommend IMARC to organizations seeking a reliable research partner.
Your service is truly exceptional. Working with the IMARC team has been a seamless and professional experience. The clarity of communication, responsiveness to queries, and consistent support at every stage made the entire engagement highly efficient. The insights shared were well-structured, practical, and perfectly aligned with our requirements, helping us make informed decisions with confidence. Overall, the dedication and professionalism demonstrated by your team stand out, and I would be glad to recommend IMARC as a reliable and trustworthy research partner.
IMARC did an outstanding job in preparing our study. They were punctual, precise, and consistently responsive throughout the entire process. The team delivered all the data we required in a clear, well-organized, and highly professional format. Their strong attention to detail, combined with their ability to meet every deadline without compromising quality, truly set them apart. Overall, their reliability and commitment made them an exceptional partner for our project, and we would gladly work with them again in the future.
IMARC made the whole process incredibly easy from start to finish. Everyone I interacted with via email was polite, professional, and straightforward to deal with, always keeping their promises regarding delivery timelines and remaining consistently solutions-focused. From my very first contact, I appreciated the professionalism and support shown by the entire IMARC team. I highly recommend IMARC to anyone seeking timely, affordable, and reliable information or advice. My experience with IMARC was excellent, and I truly cannot fault any aspect of it.
I’d like to express my sincere gratitude for the excellent work you accomplished with the study. Your ability to quickly understand our requirements and deliver high-quality results under tight timelines truly reflects your expertise, exceptional work ethic, and unwavering commitment to your customer’s success. The professionalism and responsiveness you demonstrated throughout the process made a significant difference. Our entire team and company are incredibly thankful for your dedication, reliability, and support. Once again, thank you for your outstanding contribution.