Manufacturing
October 22 2026
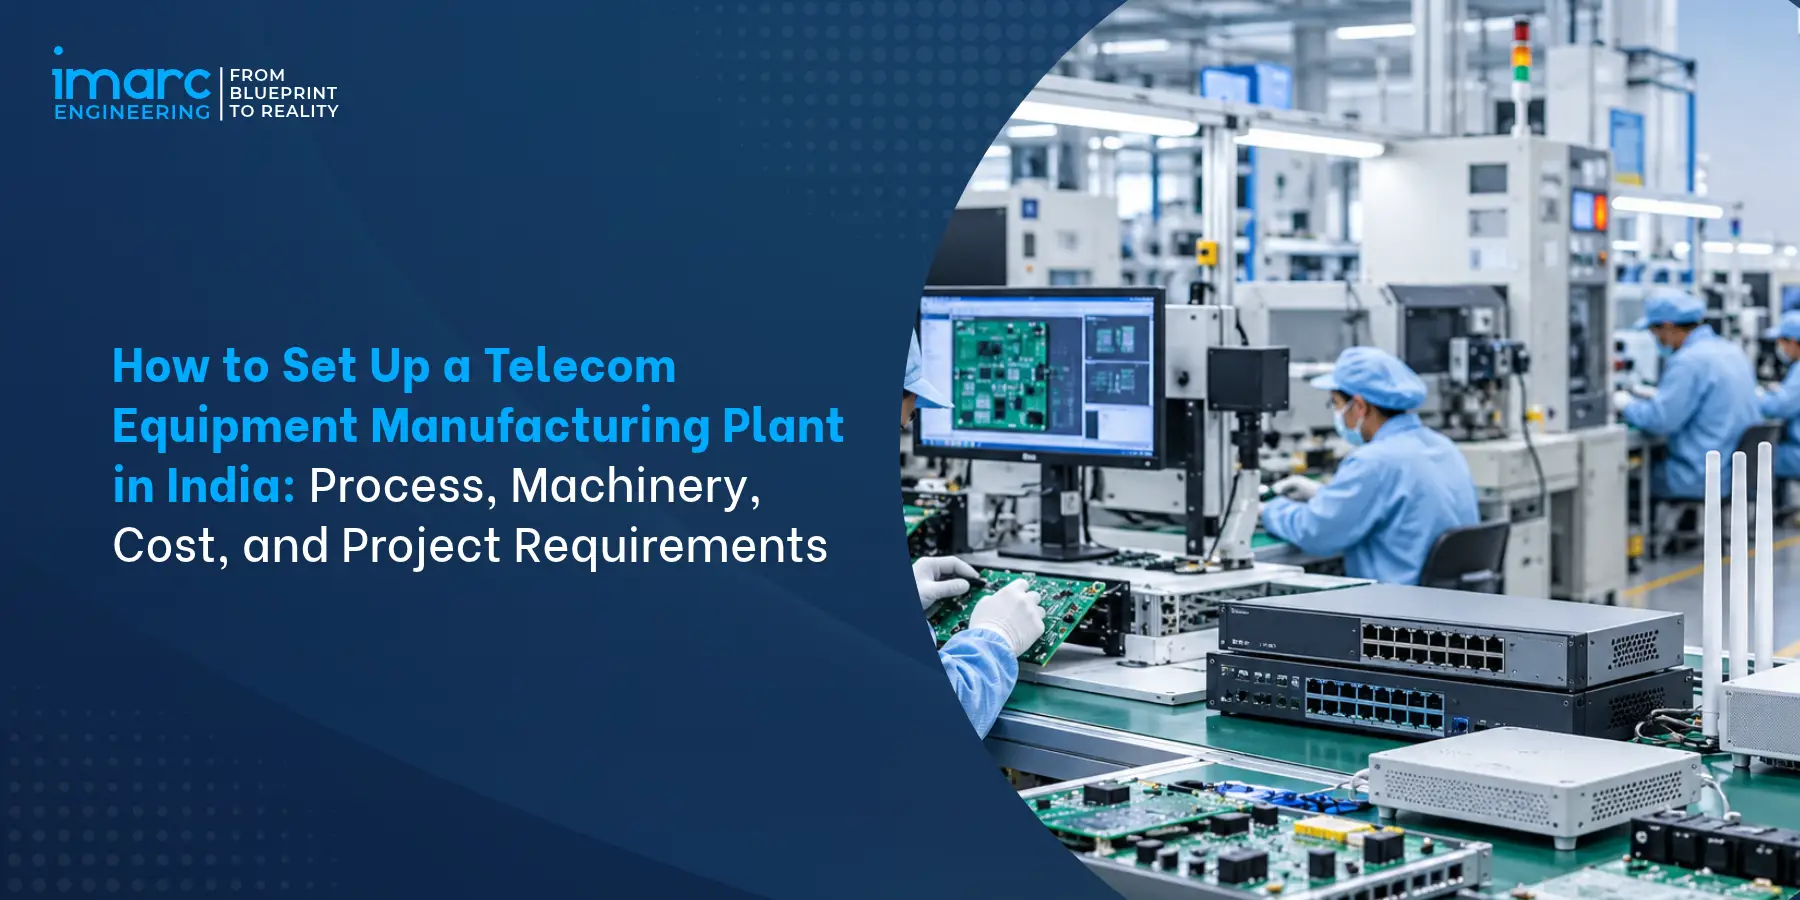
How to Set Up a Telecom Equipment Manufacturing Plant in India: Process, Machinery, Cost, and Project Requirements
Introduction
India's networks are being rebuilt in layers: 4G densification, 5G macro and small-cell rollout, fibre-to-the-home, BharatNet backhaul and data-centre interconnect. Every one of those layers consumes hardware radio units, baseband units, optical line terminals, routers, antennas, rectifiers and cable assemblies and most of that hardware has historically arrived by container from East Asia and Europe.
Procurement behaviour is changing. Public and private operators now weight domestic value addition in tenders, global OEMs have shifted radio and optical sub-assembly to Indian contract manufacturers, and incentive schemes reward depth of local manufacturing rather than final-box assembly.
For investors, project sponsors and manufacturers, a telecom equipment manufacturing plant in India is a component-sourcing, test-capacity and certification problem long before it is a sales problem. Placement equipment is standard; the differentiators are RF metrology, thermal and environmental qualification, and the regulatory stack that gates shipment.
This guide sets out the engineering and commercial architecture of a bankable facility product segmentation, SMT and RF process steps, machinery specification, cleanroom and ESD requirements, utilities, effluent, licensing and CAPEX and OPEX composition so capital is committed against verified assumptions rather than vendor brochures.
Scope of this Guide
This guide answers one question: how can investors plan and develop a telecom equipment manufacturing plant in India, from product and technology selection to approvals and commercial production? It covers the assembly and test of telecom and networking hardware radio units, baseband and switching equipment, optical transport, routers and customer premises equipment, antennas, cable assemblies and power systems and deliberately separates bare PCB fabrication from PCB assembly, finished equipment manufacture and contract manufacturing, because each carries a different capital, effluent and licensing profile.
Machinery, cleanroom classes, utility loads, land areas, certification routes and cost ranges are indicative planning figures to be replaced by vendor quotations, site data and product-specific test plans during the detailed project report stage.
Table of Contents
- Introduction
- Why a Telecom Equipment Manufacturing Plant in India Matters for Investors in 2026
- What a Telecom Equipment Manufacturing Plant in India is and Why It Matters
- How to Set Up a Telecom Equipment Manufacturing Plant in India
- Telecom Equipment Manufacturing Plant in India: Product Types and Capacity Planning
- Raw Materials, Components and Chemicals for a Telecom Equipment Manufacturing Plant in India
- Core Process Steps for a Telecom Equipment Manufacturing Plant in India: PCB Assembly and Sub-Assembly
- Core Process Steps for a Telecom Equipment Manufacturing Plant in India: RF Alignment, Testing and Certification
- Machinery, Cleanroom and Utilities for a Telecom Equipment Manufacturing Plant in India
- Effluent, Licences and Project Economics for a Telecom Equipment Manufacturing Plant in India
- Conclusion
1. Why a Telecom Equipment Manufacturing Plant in India Matters for Investors in 2026
Four structural conditions shape a disciplined telecom equipment manufacturing plant in India in 2026, and each one changes the technical configuration an investor should fund.
1.1 Import Dependence and Localisation of Telecom Hardware Manufacturing
India's network build-out has been served largely by imported base stations, optical transport and routers, with domestic content concentrated in passive hardware, cables and enclosures. That is shifting: operators increasingly weight domestic value addition in tenders, and global OEMs have moved final assembly and sub-assembly of radio units, baseband units and optical line terminals to Indian contract manufacturers.
The commercially defensible position for a new entrant is depth component-level assembly, in-house RF alignment and accredited test capability rather than screwdriver integration of imported kits, which competes purely on labour cost and captures no margin.
1.2 Policy Framework and Telecom Manufacturing Incentives
The Production Linked Incentive (PLI) Scheme for Telecom and Networking Products, administered by the Department of Telecommunications, supports eligible manufacturers based on notified investment and incremental-sales conditions. The scheme also provides differentiated treatment for certain products and design-led manufacturing.
Eligibility, product coverage, investment thresholds, incentive rates and applicable periods should be verified against the latest DoT notification before they are included in a project financial model. State electronics policies may separately provide incentives such as capital subsidies, stamp-duty concessions or power-related benefits, subject to state-specific eligibility conditions.
1.3 Investment Ecosystem and Telecom Manufacturing Companies India
The contract-manufacturing base clusters around Noida and Greater Noida, Chennai and Sriperumbudur, Pune, Bengaluru, Hyderabad and Sanand, where electronics clusters already supply trained SMT operators, test engineers and calibration laboratories. The component layer remains thin: multilayer PCBs, RF front-end modules, SAW and BAW filters, magnetics and precision connectors are still largely imported, so working capital is dominated by inbound logistics and inventory carrying cost.
Component availability and working-capital requirements depend on the bill of materials, supplier locations, allocation arrangements, import logistics and inventory strategy. Investors should obtain current lead-time and pricing information from qualified suppliers and model inventory requirements against actual procurement schedules, demand variability and customer delivery commitments.
1.4 The Cost of Poor Planning
Three planning errors can increase project cost and delay commercial production. First, installing SMT capacity without the required RF, optical or functional testing capability can leave the facility unable to complete product qualification. Second, starting production planning without assessing applicable MTCTE, BIS, and WPC requirements can delay product approval and dispatch. Third, sizing the plant around a single customer or tender can create underutilised capacity when demand changes. A product-segmented detailed project report (DPR) can help address these risks by aligning manufacturing capacity, testing infrastructure, customer demand, and regulatory requirements.
2. What a Telecom Equipment Manufacturing Plant in India is and Why It Matters
A telecom equipment manufacturing plant in India is defined by what it is licensed to build, what it can test, and where the facility boundary sits.
2.1 Definition and Facility Boundary
A telecom equipment manufacturing plant converts bare printed circuit boards, electronic components, mechanics and firmware into tested, certified network elements. The boundary is a commercial decision as much as an engineering one: an assembly-only plant buys tested sub-assemblies and performs integration and final test; an integrated plant runs SMT, through-hole, sub-assembly, RF alignment and conformance testing under one roof.
A contract manufacturing plant builds to a customer's design, bill of materials, test specification and quality plan. Product certification responsibility depends on the applicable regulatory framework, the identity of the applicant or certificate holder, brand ownership, the product's market role and the commercial agreement between the parties. The manufacturer and customer should define who will obtain and maintain each applicable approval before production begins.
2.2 PCB Fabrication, PCB Assembly, Finished Equipment and Contract Manufacturing
These are four distinct businesses. PCB fabrication etches, drills, plates and electrically tests bare boards, and is capital and effluent intensive copper and ammonia etchants, plating rinses and a full effluent treatment plant with possible zero liquid discharge. PCB assembly places and solders components on a board supplied by a fabricator, and is the core of surface mount technology. Finished equipment manufacturing adds enclosure, thermal design, cabling, RF alignment, firmware loading and certification under the seller's own brand. Contract manufacturing performs any of the above against a customer's bill of materials. Investment, licensing and working capital differ sharply across the four.
2.3 Scale Determinants for a Telecom Equipment Production Facility
Production scale depends on the product mix, component density, board complexity, changeover frequency, line availability, process yield and number of operating shifts. Effective SMT capacity should be estimated using the selected equipment's demonstrated performance for the planned product mix, rather than its headline placement speed. RF, optical and functional-test capacity should be modelled separately using expected test time per unit, available operating hours, utilisation, retesting and maintenance allowances. Annual output should be stated against a defined product mix, shift pattern and test programme. All capacity assumptions should be validated during detailed engineering and equipment selection.
2.4 Plant Sections
| Section | Function | Key Equipment |
|---|---|---|
| Incoming Inspection | Component and PCB verification | XRF, microscope, LCR meter |
| Component Store | Moisture-sensitive device control | Dry cabinets, baking ovens |
| SMT Hall | Paste printing to reflow | Printer, placer, reflow oven |
| Through-Hole Area | Connector and through-hole joints | Wave solder, selective solder |
| Sub-Assembly | Chassis, cabling, thermal build | Torque drivers, dispensing robots |
| RF Test Floor | Alignment and conformance | VNA, analysers, shielded rooms |
| Burn-In and Reliability | Environmental screening | Burn-in racks, thermal chambers |
| Packing and Dispatch | Serialisation, ESD packing | Labellers, sealers, stackers |
| Utilities Block | Power, air, nitrogen, HVAC | Chillers, compressors, DG sets |
| Effluent and Waste Yard | Treatment and scrap handling | ETP, dross separator, baler |
3. How to Set Up a Telecom Equipment Manufacturing Plant in India
Setting up a telecom equipment manufacturing plant in India requires coordinated planning across product selection, component sourcing, production technology, testing infrastructure and regulatory compliance. Investors should establish the manufacturing scope and commercial feasibility before finalising equipment purchases or facility design. The following steps outline the development process.
Step 1: Identify the Product Portfolio and Manufacturing Scope
Select the telecom products to be manufactured, such as 5G radio units, optical network terminals, routers, switches, antennas or cable assemblies. Determine whether the facility will undertake PCB assembly, finished equipment manufacturing, contract manufacturing or integrated PCB fabrication. Each model has different machinery, technical expertise, investment and certification requirements.
Step 2: Conduct a Feasibility Study and Prepare a DPR
Evaluate market demand, customer requirements, production capacity, component availability and manufacturing technology. Prepare a detailed project report (DPR) covering capital expenditure, operating costs, working capital, utility requirements, potential incentives and financial viability. Capacity planning should account for SMT line efficiency, product mix, testing time, production shifts and expected utilisation.
Step 3: Select the Location and Develop the Plant Layout
Evaluate industrial locations based on electronics supply-chain access, skilled labour, transport connectivity, power reliability and proximity to testing facilities. Develop a layout covering incoming inspection, component storage, SMT assembly, soldering, mechanical integration, RF testing, quality control and dispatch. Allocate additional space for shielded test rooms, environmental chambers and utilities where required.
Step 4: Finalise Manufacturing Technology and Machinery
Select SMT printers, pick-and-place machines, reflow ovens, inspection systems and assembly equipment based on the product design and planned throughput. Specify RF testing equipment, optical test benches, automated test systems and environmental chambers according to the product portfolio. Equipment selection should consider accuracy, production flexibility, calibration, maintenance and integration with quality-control systems.
Step 5: Establish Component Sourcing and Quality-Control Systems
Identify suppliers for PCBs, semiconductors, RF components, connectors, optical modules, enclosures and other materials. Establish component traceability, incoming inspection and inventory controls. Implement electrostatic discharge protection, moisture-sensitive component handling and appropriate environmental controls. Develop inspection and testing procedures to verify manufacturing quality and product reliability.
Step 6: Obtain Applicable Licences and Regulatory Approvals
Identify the factory, environmental, fire-safety and other statutory approvals applicable to the proposed facility. Determine whether the products require Mandatory Testing and Certification of Telecommunication Equipment (MTCTE) certification from TEC, BIS registration or Wireless Planning and Coordination (WPC) approvals. Certification requirements should be assessed by product category and incorporated into the project schedule before commercial supply.
Step 7: Install Equipment and Commission Production Lines
Complete building and utility works before installing SMT lines, assembly stations, RF test equipment and supporting systems. Conduct equipment installation, calibration, trial production and process validation. Verify soldering quality, electrical performance, RF characteristics, product traceability and environmental performance against defined acceptance criteria.
Step 8: Begin Commercial Production and Monitor Performance
Start commercial manufacturing after completing applicable approvals, product qualification and customer acceptance requirements. Monitor first-pass yield, production throughput, equipment utilisation, testing efficiency, rejection rates and manufacturing costs. Use production data and customer feedback to improve process stability, capacity utilisation and product quality.
4. Telecom Equipment Manufacturing Plant in India: Product Types and Capacity Planning
Product selection precedes plant design, because each telecom product family imposes a different board technology, test bench and certification route.
4.1 Product Categories and 5G Radio Equipment
5G radio equipment macro remote radio units, massive-MIMO active antenna units and small cells is RF-dominant: it needs high-frequency laminate, cavity or BAW filters, die-cast housings with thermal design, and over-the-air test capability. Baseband units, switches and routers are digital, placement-dense and test-bound. Optical network equipment depends on optical sub-assembly and fibre cleanliness. Antennas, cable assemblies, connectors, rectifiers and lithium battery packs are mechanically or power-electronics led. A single line configuration does not serve all of them, and a plant that claims to is usually a plant that does none well.
4.2 Optical Network Equipment and Telecom Routers
Optical line terminals and ONTs require fibre pigtail routing, connectorised or spliced interfaces, and calibration of transmit power, extinction ratio, receiver sensitivity and bit-error rate. Test benches need an optical spectrum analyser, power meter, variable optical attenuator and a traffic generator running RFC 2544 or Y.1564 throughput, latency and frame-loss tests. Routers add layer-2 and layer-3 protocol conformance and interoperability testing with real line cards. Cleanliness matters more than on radio boards: a single micron-scale particle on a fibre end-face destroys the link, so end-face inspection microscopes and cleaning kits are standard equipment.
4.3 Capacity Planning and Telecom Equipment Assembly Line Throughput
Model the plant from the test floor backwards. Capacity should be modelled using effective placement capacity, product mix, board complexity, changeovers, line availability, yield and shifts. RF and functional test capacity should then be calculated separately from test time per unit, available operating hours, utilisation and retest allowance. This is where telecom plants become capital-heavy: the test floor frequently costs as much as the SMT hall, and it is the constraint that governs revenue (Figures are indicative in nature, may vary).
4.4 Location and Cluster Selection for Telecom Manufacturing Plant Design
Site selection weighs electronics cluster depth, access to accredited test and calibration laboratories, air cargo and port proximity for imported components, power reliability, and availability of SMT operators and RF technicians. Noida, Chennai, Pune, Bengaluru and Hyderabad offer most of these, with state electronics policies adding capital subsidy and stamp duty relief. Site area and built-up area should be established from the production programme, equipment footprint, test facilities, stores, utilities, fire access, parking, future expansion and local development regulations. Radio products requiring anechoic or OTA facilities may require additional structural and space allowances.
5. Raw Materials, Components and Chemicals for a Telecom Equipment Manufacturing Plant in India
Component specification and process chemistry determine yield, field reliability and certification success far more than equipment branding does.
5.1 Base Materials and Component Kits
The bill of materials is dominated by imported content: FR-4 laminate at Tg 150-180 degrees C for digital boards, hydrocarbon-ceramic or PTFE-based laminate for RF boards above 3 GHz, and multilayer boards at 4-16 layers with impedance-controlled traces. Components include BGA and QFN baseband processors, RF power amplifiers and low-noise amplifiers, SAW and BAW filters, transceivers, FPGAs, DDR memory, magnetics, board-to-board connectors, SFP and QSFP optical modules, die-cast aluminium housings, heat sinks, fans, gaskets and cable assemblies. Component authenticity screening at goods-inward is a counterfeit-control requirement, not a formality.
5.2 Solder Paste, Fluxes and Process Chemistry
Solder paste, flux and solder-alloy selection should reflect component requirements, PCB design, joint reliability, assembly process and customer specifications. Lead-free alloys such as SAC305 may be suitable for some applications, but alloy composition, powder type, stencil design and metal content should be selected for the intended process and component pitch. Reflow and wave-soldering conditions should be established through material datasheets, equipment capability and process validation. Conformal coatings and thermal interface materials should be selected according to the operating environment, thermal requirements, material compatibility and product reliability targets. Where cleaning is required, the cleaning process and residue acceptance criteria should be validated for the chosen flux and assembly.
5.3 Consumables and Specifications
Recurring consumables may include stencils, squeegee blades, placement nozzles, feeder components, approved cleaning agents, ESD-safe packaging, desiccants and humidity indicator cards. Nitrogen may be required for selected soldering processes. Stencil dimensions and consumable specifications should be determined by PCB design, component pitch and process capability. Moisture-sensitive devices should be handled in accordance with their moisture sensitivity level (MSL), the applicable J-STD-033 requirements and the component manufacturer's instructions. Storage conditions, floor life, baking requirements and handling limits should be documented and controlled through the facility's validated process.
5.4 Chemical Storage, Handling and Safety
Solder paste, fluxes, cleaning agents and conformal-coating materials should be stored and handled according to their safety data sheets, manufacturer instructions and applicable fire, environmental and occupational-safety requirements. Storage temperature, shelf life and acclimatisation time for solder paste should follow the specific product datasheet. Flammable solvents may require designated ventilated storage, suitable fire protection, and controls against ignition sources. Where coating or cleaning processes release volatile organic compounds or other hazardous substances, assess the need for local exhaust ventilation, emissions controls and worker-exposure monitoring. Maintain current safety data sheets, chemical inventories, and documented handling procedures.
6. Core Process Steps for a Telecom Equipment Manufacturing Plant in India: PCB Assembly and Sub-Assembly
The production flow runs from paste printing to serialised sub-assembly through four controlled stages, each with parameters that must be fixed in the equipment specification.
6.1 Solder Paste Printing and Solder Paste Inspection
Boards enter a controlled solder-paste printing area where a stencil printer aligns the PCB with the stencil using the equipment's vision system. Printer settings, including alignment tolerance, squeegee pressure, print speed and stencil aperture design, should be established through PCB design requirements, equipment capability and process validation. Solder paste inspection may be used to verify deposit coverage, volume, height and alignment, with inspection coverage and acceptance limits based on component pitch, product criticality, customer requirements, and the qualified process. A cleanroom classification should be specified only where justified by product, process or customer requirements; it is not a universal requirement for solder-paste printing.
6.2 Component Placement and Reflow Soldering
Component placement equipment should be selected according to PCB dimensions, component types, placement accuracy, effective throughput and changeover requirements. High-speed placement machines handle passive components, while precision placement systems accommodate fine-pitch devices, including QFN and BGA packages.
Reflow parameters should follow the solder-paste manufacturer's recommendations, PCB construction, component thermal limits and product reliability requirements. The validated process should control ramp rate, soak, peak temperature, time above liquidus and atmosphere, as applicable.
6.3 Automated Optical Inspection, X-Ray and Rework
X-ray inspection may be used for BGA, LGA and other hidden solder joints where required. Void limits and acceptance criteria should be defined according to component type, thermal/electrical requirements, customer specifications and the qualified manufacturing process. In-circuit test or flying-probe test verifies nets and values, and boundary scan covers JTAG-capable devices.
Rework runs on a hot-air station with bottom-side preheating; BGA reballing is performed only where the process is qualified and profiled, because unqualified rework is the most common source of early field failure in telecom hardware.
6.4 Mechanical Integration, Cabling and Enclosure Assembly
Assembled boards move to sub-assembly, where housings, heat sinks, thermal pads, gaskets, fans and connectors are installed using torque-controlled tools. Fastener torque values follow manufacturer specifications and validated assembly procedures. RF jumper cables are routed within specified bend-radius limits, and connector torque is verified using calibrated tools.
For outdoor telecom equipment, applicable ingress-protection requirements, such as IP65 or IP66, are verified through appropriate testing. Each unit is serialised, with relevant identifiers, firmware versions and component traceability recorded for quality control, warranty and audit purposes.
7. Core Process Steps for a Telecom Equipment Manufacturing Plant in India: RF Alignment, Testing and Certification
Finishing and verification turn assembled hardware into a certified, shippable network element that operators and regulators will accept.
7.1 RF Alignment and Board-Level Calibration
RF boards are aligned on conducted test benches pairing a vector signal generator, a vector network analyser, a spectrum analyser and a calibrated power meter through a programmable attenuator bank and a shielded test fixture. Technicians set transmit power, gain flatness across the band, error vector magnitude, adjacent-channel leakage ratio and return loss.
Bench calibration is traceable to national standards, and cable and connector losses are compensated in software. An uncalibrated bench is the single largest source of false passes in a radio plant, and calibration interval management is a hard quality-system requirement.
7.2 5G Equipment Manufacturing India: Conformance and OTA Testing
Sub-6 GHz 5G new radio units are tested against 3GPP TS 38.141 base station conformance, covering output power, modulation quality, unwanted emissions and receiver reference sensitivity. Where conducted access is unavailable or insufficient, active antenna systems and other applicable radio products may require over-the-air (OTA) testing in an anechoic chamber or compact antenna test range.
The test method and facility configuration should reflect the product's frequency range, antenna characteristics, measurement requirements and applicable conformance specifications. Chamber procurement, installation time and space requirements depend on the selected system, shielding and absorber design, site conditions, calibration needs and supplier schedule. These requirements should be established with the test-equipment supplier during facility planning.
7.3 Environmental, Reliability and Telecom Product Testing
Products are qualified under IEC 60068 for dry heat, damp heat, vibration and shock, IEC 60529 for IP65 and IP66 ingress, and IEC 60068-2-52 for salt mist on outdoor units. Electromagnetic compatibility follows CISPR 32 and IEC 61000-4-2, -4-4, -4-5 and -4-6 for immunity; safety follows IEC 62368-1; and telecom reliability programmes often reference Telcordia GR-63 and GR-1089. Burn-in, environmental screening and reliability testing should be defined according to the product specification, applicable TEC/MTCTE requirements, customer qualification requirements and the manufacturer's reliability programme.
7.4 MTCTE, TEC Certification and BIS Standards
Notified telecom equipment supplied, imported or used in India is subject to the Mandatory Testing and Certification of Telecommunication Equipment (MTCTE) framework administered by the Telecommunication Engineering Centre (TEC). Certification is based on the Essential Requirements applicable to the relevant equipment category, including technical, safety, EMI/EMC and security requirements where specified. The current list of notified equipment and applicable requirements should be checked for each product before launch.
MTCTE certification is generally linked to the certified model, but the procedure also provides for associated models and equipment families subject to specified conditions. Separate BIS requirements may apply where the product falls within a notified BIS/MeitY compulsory-registration category. Wireless products may require WPC approvals, including Equipment Type Approval (ETA), depending on their frequency band, application and regulatory classification. Separate WPC spectrum or site-related approvals, including SACFA clearance, may apply where the product is deployed as part of a wireless installation requiring such clearance.
8. Machinery, Cleanroom and Utilities for a Telecom Equipment Manufacturing Plant in India
Machinery, controlled environments and utilities account for the majority of capital and almost all of the technical risk in a telecom equipment manufacturing plant in India.
8.1 Telecom Manufacturing Machinery: Selection Drivers
Specify placement equipment on accuracy at three sigma, feeder capacity and changeover time rather than quoted speed, because a 60,000 components-per-hour machine losing 40 minutes per changeover on a high-mix plant delivers less than a 35,000 machine with fast trolleys. Specify reflow ovens on zone count, atmosphere control and profile repeatability; test equipment on measurement uncertainty and calibration interval; chambers on quiet-zone performance and frequency range. Guarantees should be tied to first-pass yield and test-time targets, not throughput alone.
8.2 Cleanroom Requirements and ESD Protection
SMT, optical assembly and RF testing areas should be designed around the contamination sensitivity of the product and process rather than a universal cleanroom classification. Where controlled environments are required, the applicable ISO 14644 classification should be established from product, process and customer requirements.
ESD control should be incorporated throughout component handling, assembly, testing and packaging in accordance with the applicable ESD control programme and product sensitivity. Grounded workstations, suitable flooring, wrist straps, ionisation where required, ESD-safe material handling and protective packaging should be selected based on the facility's ESD risk assessment and quality requirements.
8.3 Utilities: Power, Water, Gases and HVAC
Utility requirements should be developed from the equipment list, production schedule, environmental conditions and reliability philosophy. The electrical load should include SMT equipment, RF and electrical test systems, HVAC, compressed air, nitrogen generation or storage, IT systems, lighting, utilities and redundancy requirements. Compressed-air quality, nitrogen purity, cooling capacity and backup power should be specified from individual equipment and process requirements rather than assumed as fixed plant-wide values.
8.4 Plant Layout and Material Handling
The layout should support an efficient flow from receiving and incoming inspection through component storage, SMT, through-hole assembly, sub-assembly, RF or optical testing, packing and dispatch. Separate areas where required by contamination control, ESD protection, product sensitivity, safety or test conditions. Airlocks may be appropriate where a defined environmental-control strategy requires them, while shielded rooms may be needed for particular RF measurements. Material handling may use ESD-safe trolleys, board magazines, conveyors or automated guided vehicles (AGVs), depending on throughput, travel distances, labour availability and the business case for automation. Storage systems, equipment foundations, conveyor routes and utility penetrations should be coordinated with the final layout before construction.
8.5 Key Machinery
| Category | Equipment | Key Selection Parameters |
|---|---|---|
| Paste Printing | Vision stencil printer | PCB size, printing accuracy, changeover time |
| Paste Inspection | 3D solder paste inspection | Inspection coverage, resolution, cycle time |
| Placement | Pick-and-place machines | Product mix, component range, effective placement capacity |
| Reflow | 10-zone nitrogen convection oven | Thermal profile, throughput, atmosphere requirements |
| Inspection | 3D AOI and 2D/3D X-ray | Inspection resolution, defect coverage, cycle time |
| Electrical Test | ICT, flying probe, JTAG | Test coverage, fixtures, product complexity |
| RF Test | VNA, analysers, shielded rooms | Frequency range, measurement accuracy, test time |
| Conformance | OTA anechoic chamber, thermal chamber | Product dimensions, applicable standards, test requirements |
9. Effluent, Licences and Project Economics for a Telecom Equipment Manufacturing Plant in India
Effluent, residues and approvals determine whether an otherwise sound telecom equipment manufacturing plant in India is ever allowed to run at design capacity.
9.1 Effluent, Emissions and Electronic Waste
Telecom assembly plants generally generate limited process effluent compared with PCB fabrication facilities. Cleaning wastewater, soldering residues, solvent wastes and other streams should be characterised and managed according to their composition and the applicable environmental permissions. Where PCB fabrication is included, copper-bearing etchants, plating solutions and rinses can create substantially more complex wastewater-treatment requirements. Treatment technology and discharge limits should be established from the process chemistry, discharge route and State Pollution Control Board consent conditions.
9.2 Telecom Equipment Manufacturing Licence and Approvals
Regulatory requirements for a telecom equipment manufacturing plant depend on the products manufactured, the activities performed and the applicable central and state regulations. Approvals may include State Pollution Control Board permissions, factory and occupational safety registrations, fire and building approvals, and hazardous waste authorisation, where applicable.
Additional requirements may include E-Waste Rules registration for entities covered by the rules, an Importer Exporter Code (IEC) for relevant import or export activities, TEC's MTCTE certification for notified telecom equipment, BIS certification for products covered by applicable compulsory certification orders, and WPC approvals for relevant wireless equipment.
Requirements for boilers, pressure equipment and other specialised installations should be assessed only where such equipment is used. Before commissioning, prepare a project-specific compliance matrix identifying each applicable approval, the responsible entity, the issuing authority and the required application or renewal timeline.
9.3 CAPEX and OPEX Composition
CAPEX should be developed from the selected product mix, SMT and assembly equipment, RF and functional-test infrastructure, environmental chambers, ESD and environmental controls, utilities, buildings, IT/traceability systems, certification facilities, installation, engineering and contingency. OPEX should be modelled primarily from the product bill of materials, labour, utilities, quality and testing, logistics, inventory carrying costs, maintenance and overheads.
9.4 Project Timelines and Risk Register
Project duration depends on site readiness, statutory approvals, building and utility works, equipment procurement, installation, validation, product qualification and certification. Radio facilities with specialised RF or OTA infrastructure can require additional procurement and commissioning time. The critical path should be established through a project-specific implementation schedule. Risks to register explicitly are certification failure on a product variant, customer qualification audits, component allocation, foreign exchange exposure on imported bills of materials, and single-customer concentration in operator tenders.
9.5 Strengthen Project Economics
Telecom manufacturing project cost varies significantly with product mix, production capacity, PCB fabrication scope, SMT automation, RF and OTA testing, certification infrastructure, land and building costs, utilities and working-capital requirements. A reliable investment estimate should therefore be developed from a project-specific equipment list, site assumptions, production programme, vendor quotations and detailed engineering rather than a generic industry cost range.
Financial feasibility should also evaluate production utilisation, component costs, first-pass yield, testing expenses, certification costs, inventory requirements, and customer payment terms. The DPR should include projected cash flows, break-even analysis, working-capital requirements, and sensitivity scenarios covering changes in demand, component pricing, foreign exchange rates, and production efficiency.
Conclusion
A bankable telecom equipment manufacturing plant in India is a test-capacity business wrapped around an assembly line. Placement equipment is commoditized and financeable; what is scarce is accredited RF metrology, thermal and environmental qualification, and a certification pipeline that runs ahead of the production ramp rather than behind it.
Investors who treat product selection, test strategy, cleanroom and ESD design, utility sizing and the MTCTE and BIS calendar as one integrated design problem get a facility that can flex between radio, optical and routing products as tenders shift. Investors who purchase machinery before finalising product specifications, testing requirements and facility design risk costly modifications, project delays and additional capital expenditure during commissioning.
The three priorities are unambiguous. First, segment the product portfolio before sizing anything, because a 5G radio unit and an optical network terminal share an SMT line but not a test floor, a certification route or a margin structure. Second, build the test and calibration capability at the same time as the assembly hall, since radio and optical products cannot be shipped without it and retrofitting chambers into a finished building is both expensive and slow. Third, treat MTCTE certification, BIS registration and WPC approval as critical-path activities running in parallel with engineering, not as post-commissioning paperwork. Everything else automation level, building finish, equipment brand is negotiable.
PURSUING A TELECOM EQUIPMENT MANUFACTURING PLANT IN INDIA?
IMARC Engineering supports investors, project sponsors and manufacturers with product-mix and capacity planning, site selection, plant layout, equipment selection, cleanroom and ESD design, utilities planning, RF test-floor configuration, effluent treatment, regulatory approvals, incentive-scheme structuring and capital investment planning. The advisory covers radio units, baseband and switching equipment, optical transport, routers, customer premises equipment and cable assemblies, including SMT assembly, through-hole soldering, mechanical integration, RF alignment, conformance testing and MTCTE certification, with project-specific infrastructure and commissioning planning.
→ Schedule a telecom equipment manufacturing scoping consultation with an IMARC specialist
Frequently Asked Questions
Start with the product portfolio: decide whether you are building radio units, optical transport, routers or cable assemblies, since each fixes board technology, test benches and certification route. Prepare a DPR covering product mix, capacity at defined test times, machinery, layout, utilities and cost; secure industrial land and SPCB consent; then commission SMT and test lines and complete MTCTE certification before commercial dispatch.
5G macro radio units, massive-MIMO active antenna units and small cells; baseband units; optical line terminals, ONTs and DWDM transponders; routers, switches and customer premises equipment; microwave backhaul; antennas; optical and copper cable assemblies; connectors; rectifiers and lithium battery packs; and enclosures. Products differ sharply in board technology, test floor requirement and certification route, so portfolio selection precedes plant design.
A typical line runs a vision stencil printer, 3D solder paste inspection, a chip shooter and fine-pitch placer, a ten-zone nitrogen reflow oven, 3D AOI, 2D or 3D X-ray, in-circuit and flying-probe test, boundary scan, RF benches with vector network and signal analysers, shielded test rooms, an OTA anechoic chamber for radio products, thermal chambers, burn-in racks, torque-controlled assembly tools and ESD-protective material handling.
The investment depends on the product portfolio, annual capacity, SMT automation, RF and functional-test requirements, OTA facilities, building and utility requirements, certification infrastructure, land and working capital. A project-specific DPR should establish CAPEX and OPEX from equipment specifications, site assumptions and vendor quotations rather than relying on a generic cost range.
5G equipment manufacturing involves PCB assembly, solder paste printing, component placement, reflow soldering, inspection and electrical testing. Radio equipment also requires RF calibration, mechanical integration, firmware loading and product-specific conformance testing. Environmental and reliability testing may be necessary depending on the equipment design, applicable standards and customer requirements.
MTCTE, administered by TEC, applies to telecom equipment covered by its notified requirements. BIS certification is separate and applies to products covered by relevant compulsory certification orders. WPC approvals, including ETA or other permissions, may apply to wireless products depending on their specifications and use. Check each product's applicable requirements separately, as not every product needs all three.
The Production Linked Incentive scheme for telecom and networking products, administered by the Department of Telecommunications, rewards incremental sales above an investment threshold for specified product categories, with a design-led incentive component. Component-focused schemes and state electronics policies add capital subsidy, stamp duty exemption and power tariff relief. Product coverage, rates and application windows are revised periodically and must be verified against the current notification before financial modelling.
Land and infrastructure requirements depend on product mix, production capacity, SMT and assembly equipment, RF and OTA testing, stores, utilities, fire access, parking and future expansion. Radio products requiring specialised RF or OTA facilities may require additional building height, structural loading, shielding and equipment space. Electrical, HVAC, compressed air and gas requirements should be established from the detailed equipment and utility schedules.
Key challenges include imported components, supplier availability, working capital, specialised RF and optical testing, product qualification, certification, customer concentration, tender fluctuations, foreign-exchange exposure and testing infrastructure costs. Cleanroom and ESD requirements depend on the product, process and customer specifications. A feasibility study should assess these risks, production capacity, supplier commitments, testing needs and applicable MTCTE, BIS and WPC requirements.
They segment the product portfolio, build capacity models around test times rather than placement speed, specify SMT and RF test equipment with acceptance criteria, design layout, cleanroom, ESD and utility systems to ANSI/ESD S20.20 and ISO 14644, sequence MTCTE, BIS and WPC approvals, structure CAPEX and OPEX and incentive claims, and manage procurement, construction, installation and commissioning under EPCM delivery.
Recent Post
Trusted by Industry Leaders
We partner with global enterprises and ambitious businesses across sectors to deliver operational excellence, strategic insights, and sustainable growth through integrated solutions.
Success in Their Words
Real feedback from clients across industries. Discover how our solutions delivered measurable impact and operational excellence.
I wanted to express my sincere appreciation for your efforts in handling this matter. Your dedication and commitment have been truly commendable, and it is evident that you have put in tremendous hard work and expertise into resolving the issues at hand. We are greatly interested in continuing our collaboration with you in the future, as your professionalism and reliability have made you a trusted partner. Thank you once again for your invaluable contribution. We look forward to strengthening our partnership ahead.
It has been a pleasure working with the IMARC team. The insights provided were structured, clear, and highly valuable, helping us strengthen both our technical and financial planning with confidence. We deeply appreciate the team’s professionalism, responsiveness, and attention to detail throughout the engagement. Every requirement was well understood and effectively incorporated, resulting in a comprehensive and actionable output. Overall, our experience has been excellent, and I would gladly recommend IMARC to organizations seeking a reliable research partner.
Your service is truly exceptional. Working with the IMARC team has been a seamless and professional experience. The clarity of communication, responsiveness to queries, and consistent support at every stage made the entire engagement highly efficient. The insights shared were well-structured, practical, and perfectly aligned with our requirements, helping us make informed decisions with confidence. Overall, the dedication and professionalism demonstrated by your team stand out, and I would be glad to recommend IMARC as a reliable and trustworthy research partner.
IMARC did an outstanding job in preparing our study. They were punctual, precise, and consistently responsive throughout the entire process. The team delivered all the data we required in a clear, well-organized, and highly professional format. Their strong attention to detail, combined with their ability to meet every deadline without compromising quality, truly set them apart. Overall, their reliability and commitment made them an exceptional partner for our project, and we would gladly work with them again in the future.
IMARC made the whole process incredibly easy from start to finish. Everyone I interacted with via email was polite, professional, and straightforward to deal with, always keeping their promises regarding delivery timelines and remaining consistently solutions-focused. From my very first contact, I appreciated the professionalism and support shown by the entire IMARC team. I highly recommend IMARC to anyone seeking timely, affordable, and reliable information or advice. My experience with IMARC was excellent, and I truly cannot fault any aspect of it.
I’d like to express my sincere gratitude for the excellent work you accomplished with the study. Your ability to quickly understand our requirements and deliver high-quality results under tight timelines truly reflects your expertise, exceptional work ethic, and unwavering commitment to your customer’s success. The professionalism and responsiveness you demonstrated throughout the process made a significant difference. Our entire team and company are incredibly thankful for your dedication, reliability, and support. Once again, thank you for your outstanding contribution.