Manufacturing
October 23 2026
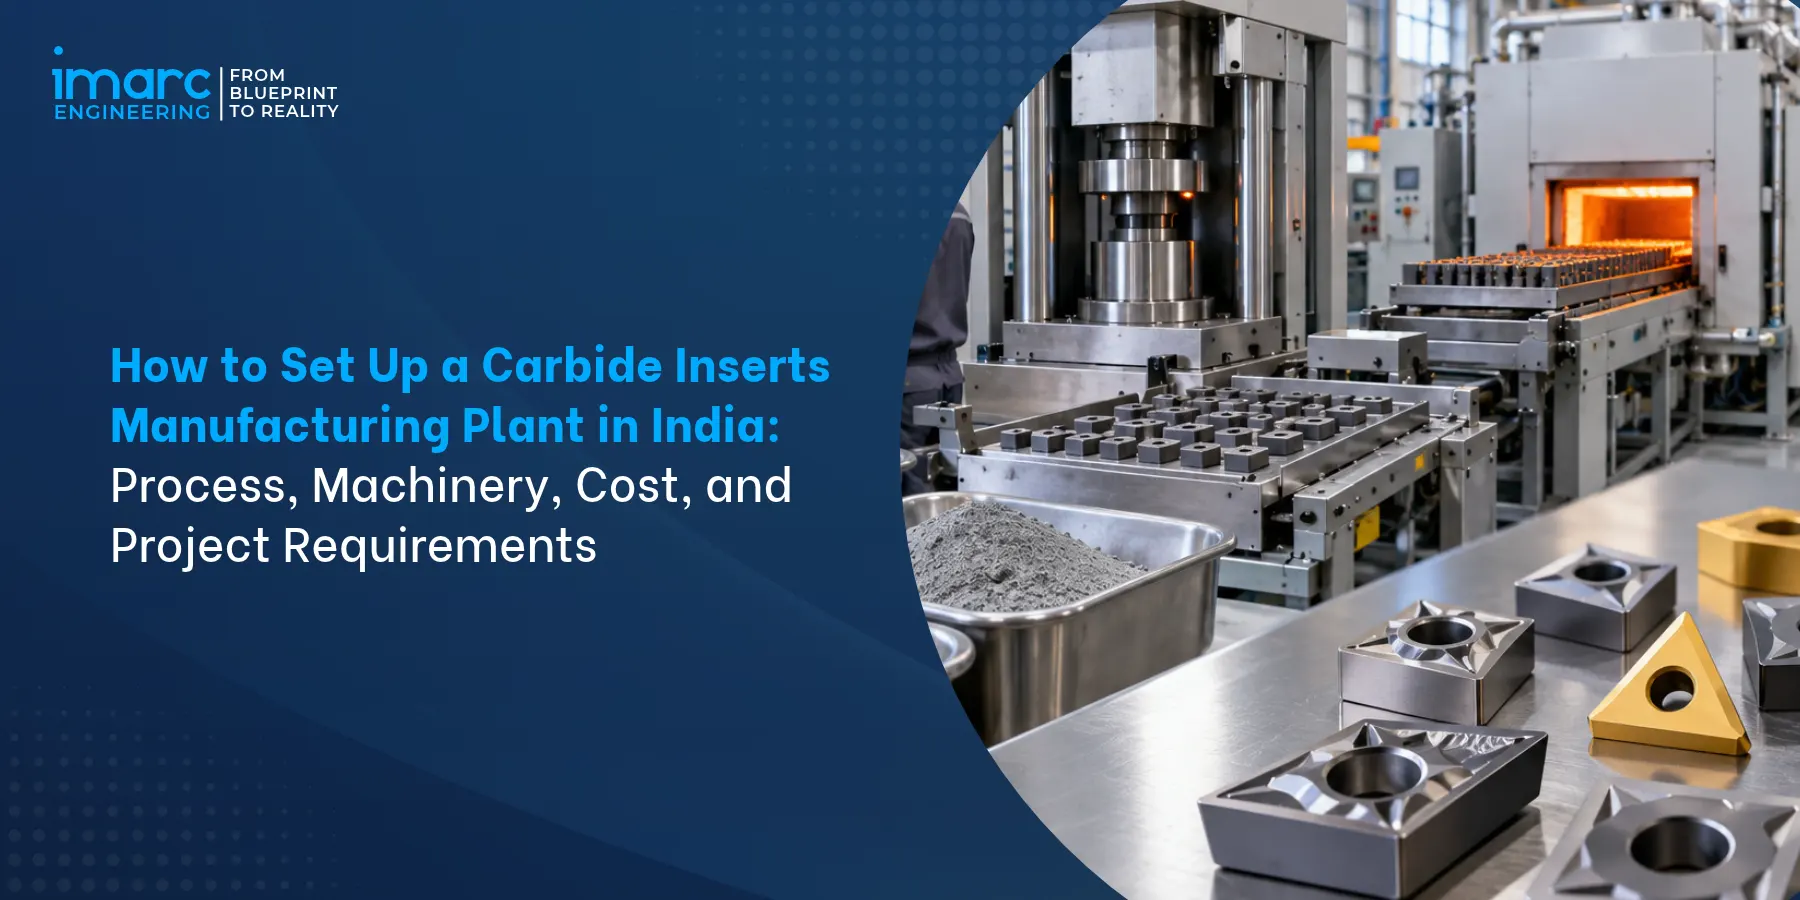
How to Set Up a Carbide Inserts Manufacturing Plant in India: Process, Machinery, Cost, and Project Requirements
Introduction
India's automotive, aerospace, railway, die-and-mould and general engineering sectors use cemented carbide inserts for a wide range of metal-cutting operations. Establishing a manufacturing facility requires careful planning of raw materials, powder metallurgy, precision grinding, coating technology, quality control, and occupational safety. Investors should assess domestic and international sourcing options, manufacturing capabilities and customer qualification requirements before committing capital.
For investors, the key decisions are which production model to adopt, which insert grades to manufacture, and how to configure machinery, utilities, environmental controls and testing facilities. This guide examines the main manufacturing routes, equipment requirements, regulatory considerations and project-cost factors for establishing a carbide inserts manufacturing plant in India. All technical parameters and investment assumptions should be validated against the selected product mix, supplier specifications, and project-specific engineering studies.
Scope of this Guide
This guide answers one question: how can investors plan and establish a carbide inserts manufacturing plant in India, from powder metallurgy and machinery selection to plant engineering, approvals and commercial production? It covers cemented tungsten carbide cutting inserts only turning, milling, grooving, threading and drilling grades and deliberately separates full powder-to-finished-insert manufacturing, purchased-blank finishing, and coating-only operations, because each carries a different capital, effluent and licensing profile. Process steps, machine specification, cleanroom classes, utility loads, land areas, approval routes and cost ranges are indicative planning figures, not quotations.
Table of Contents
- Introduction
- Why a Carbide Inserts Manufacturing Plant in India Matters for Investors in 2026
- What a Carbide Inserts Manufacturing Plant in India is and Why It Matters
- How to Set Up a Carbide Inserts Manufacturing Plant in India
- Carbide Inserts Manufacturing Plant in India: Insert Types and Capacity Planning
- Raw Materials and Chemicals for a Carbide Inserts Manufacturing Plant in India
- Core Process Steps for a Carbide Inserts Manufacturing Plant in India: Powder Preparation to Sintering
- Core Process Steps for a Carbide Inserts Manufacturing Plant in India: Grinding, Coating and Inspection
- Machinery, Cleanroom and Utilities for a Carbide Inserts Manufacturing Plant in India
- Effluent, Licences and Project Economics for a Carbide Inserts Manufacturing Plant in India
- Conclusion
1. Why a Carbide Inserts Manufacturing Plant in India Matters for Investors in 2026
Four structural conditions shape a disciplined carbide inserts manufacturing plant in India in 2026, and each one changes the technical configuration an investor should fund.
1.1 Import Dependence and Localization of Cemented Carbide Inserts
India builds a broad range of machine tools and tool holders but captures a narrow share of the coated inserts they consume, and almost none of the upstream powder. Raw-material sourcing, imported equipment and competition from established insert manufacturers are important considerations when evaluating a carbide inserts manufacturing project in India. Investors should assess domestic and international supply options for tungsten carbide powder, binder materials, machinery and finished inserts. Import dependence and procurement lead times should be quantified using current trade data, supplier quotations and the proposed product mix.
1.2 Policy Framework and Incentive Structure for Carbide Insert Manufacturing
Support is layered rather than singular. State industrial development policies typically offer capital subsidy on plant and machinery, stamp duty and registration reimbursement, SGST reimbursement and power tariff relief for continuous-process metallurgy, with thresholds, ceilings and disbursement mechanics that differ by state and are revised periodically. MSME and Udyam-linked schemes support term lending and technology upgrading, and the customs duty structure on imported carbide powder, coated inserts and PVD targets materially shifts the make-versus-buy arithmetic. Every incentive must be verified against the current notification and the project's own HS classification before it is entered into a financial model.
1.3 Investment Ecosystem and the Indian Tooling Cluster
Carbide tooling clusters where machine-tool builders, die-and-mould shops, diamond-wheel suppliers and vacuum heat treaters already operate: Coimbatore, Bengaluru, Pune, Rajkot, Ahmedabad, Ludhiana, Hyderabad and the Faridabad-Gurugram belt. These locations supply trained insert grinders and powder metallurgists, NABL-accredited calibration and testing laboratories, and service engineers for vacuum furnaces and coating chambers. Proximity to the customer base matters more than land price, because inserts are consumables sold on demonstrated tool life and delivery response, not on freight economics.
1.4 The Cost of Poor Planning
Three planning risks deserve particular attention. First, mismatched capacities across pressing, sintering, grinding, coating and inspection can create work-in-progress bottlenecks and limit saleable output. Second, inadequate cobalt-dust containment and local exhaust ventilation can increase occupational exposure and compliance risks. Third, sizing production around furnace or press nameplate capacity rather than qualified output can lead to underutilized equipment. A process-wise capacity model should identify the actual constraint using validated cycle times, equipment availability, yield, changeovers and maintenance requirements.
2. What a Carbide Inserts Manufacturing Plant in India is and Why It Matters
A carbide inserts manufacturing plant in India is defined by what it is licensed to produce, what it can measure, and where the facility boundary sits.
2.1 Definition and Facility Boundary
A cemented carbide insert plant converts tungsten carbide powder and a cobalt binder into densified, ground and coated indexable inserts of a controlled geometry. The boundary is a commercial decision as much as an engineering one: a powder plant makes ready-to-press granulate; a blank producer presses and sinters; a finisher grinds purchased blanks to ISO geometry; a coater applies PVD or CVD layers on customer-supplied inserts. Each boundary carries a different effluent profile, licence set and margin structure, and it must be drawn before any consent application is filed.
2.2 Full Powder-to-Insert, Blank Finishing and Coating-Only Models
Carbide insert manufacturing can follow three production models. Fully integrated plants combine powder preparation, pressing, sintering, grinding, inspection and coating. This model requires substantial process expertise, equipment investment and environmental controls.
Blank-finishing facilities purchase sintered carbide blanks and perform precision grinding, edge preparation and inspection. Coating may be performed in-house or outsourced. This model avoids investment in powder preparation and sintering but depends on reliable blank suppliers.
Coating-only facilities process pre-ground inserts using suitable PVD or CVD technologies. Their requirements focus on surface preparation, coating quality, process control and customer qualification. Each model should be evaluated against target markets, technical capabilities and investment requirements.
2.3 Scale Determinants for a Carbide Inserts Production Facility
Plant capacity depends on product mix, grinding time per insert, pressing-tool configuration, sintering cycle, usable furnace load, and coating chamber capacity. These parameters vary by insert geometry, grade, equipment, and process route. Capacity should be calculated as qualified saleable inserts per period, using vendor-validated cycle times, realistic utilisation, yield, changeovers and planned maintenance. Capacity should always be stated as qualified inserts per month at a defined mix, never as tonnes of powder per year (Figures are indicative in nature, may vary).
2.4 Plant Sections
| Section | Function | Key Equipment |
|---|---|---|
| Powder store | Sealed storage of WC and Co | Glove box, sealed bins |
| Powder preparation | Milling, mixing, granulation | Attritor mill, spray dryer |
| Compaction | Green insert pressing | 160-400 t hydraulic press |
| Sintering and HIP | Densification, pore closure | Vacuum furnace, HIP vessel |
| Grinding and edge prep | Geometry, tolerance, honing | 5-axis CNC insert grinder |
| Coating | Wear-resistant surface layers | PVD arc coater, CVD reactor |
| Quality laboratory | Grade and geometry release | Hardness, TRS, CMM |
| Utilities | Power, water, gases, vacuum | Chillers, compressors, argon bank |
| Effluent treatment | Cobalt and sludge removal | Settling tank, filter press |
| Packing and dispatch | Labeling and traceability | Laser marker, packing line |
3. How to Set Up a Carbide Inserts Manufacturing Plant in India
Step 1: Select the Production Model
Choose between integrated powder-to-insert manufacturing, purchased-blank finishing and coating-only operations. Assess the technical complexity, machinery requirements, investment needs and target customers for each model.
Step 2: Conduct Market and Technical Feasibility
Evaluate domestic demand, competitor offerings, customer qualification requirements and potential applications. Assess technology availability, production risks and the commercial viability of the selected manufacturing route.
Step 3: Define Product Grades and Capacity
Identify target insert geometries, carbide grades, coating requirements and production volumes. Develop a process-wise capacity model using validated cycle times, equipment utilisation and expected yields.
Step 4: Prepare the Detailed Project Report
Develop a DPR covering technology selection, raw materials, site requirements, plant layout, machinery, utilities, CAPEX, OPEX, financial projections, project risks and implementation schedules.
Step 5: Finalise Site Selection and Regulatory Requirements
Evaluate industrial locations based on infrastructure, skilled labour, logistics and environmental suitability. Identify applicable factory, pollution-control, building, fire-safety and gas-storage approvals.
Step 6: Select Technology and Procure Machinery
Evaluate equipment suppliers against production requirements, quality specifications, automation, maintenance support and acceptance criteria. Finalise procurement contracts and delivery schedules.
Step 7: Complete Plant Engineering and Installation
Develop the detailed layout, process utilities, ventilation, material handling and safety systems. Execute civil works, install equipment and integrate production and quality-control systems.
Step 8: Commission and Validate Production
Conduct equipment trials, process validation, product testing and customer qualification. Verify operational safety, product consistency and achievable production capacity before commercial dispatch.
4. Carbide Inserts Manufacturing Plant in India: Insert Types and Capacity Planning
Insert geometry and grade portfolio decide the plant configuration before capacity is fixed, because each product family consumes different grinding time, tooling and coating cycles.
4.1 Insert Geometries and ISO Designation
Indexable inserts are designated under ISO 1832 for example CNMG 120408, a rhombic 80-degree negative insert of 12.7 mm inscribed circle and 4.76 mm thickness with a 0.8 mm corner radius and classified for application under ISO 513 into P (steel), M (stainless), K (cast iron), N (non-ferrous), S (superalloy) and H (hardened) groups. A commercial portfolio spans turning, milling (APKT, ADKT), grooving, threading and drilling inserts, plus solid carbide drills and end mills where the plant elects to extend beyond indexable tooling.
4.2 Capacity Planning and Insert Throughput
Model capacity across the planned insert mix using validated machine cycle times, usable batch loads, operating schedules, changeovers, maintenance, utilisation and yield. Estimate sintering output from usable furnace capacity and cycle duration, and grinding output from qualified cycle time per insert and available machine hours. Include coating and inspection capacity where applicable. Compare all stages on a consistent basis of saleable inserts per period to identify the actual production bottleneck.
4.3 Product Mix and Grade Portfolio
Grade design matters more than tonnage. A substrate portfolio of 6-12 cobalt levels between 6% and 12%, with grain sizes from 0.5 to 2.0 micrometers and inhibitor additions for fine-grain toughness, covers most of the P, M and K map; coated grades then multiply the matrix by layer architecture. A plant entering with three grades and one coating will defend a narrow application band, while a portfolio of ten grades with two PVD and two CVD recipes supports distributor channels and OEM qualification.
4.4 Location, Cluster and Site Selection
Site selection should consider proximity to customers and suppliers, industrial infrastructure, skilled labour, electricity reliability, gas availability, environmental compliance and logistics.
Land and building requirements depend on production capacity, equipment dimensions, material handling, utility systems, storage and future expansion. Integrated manufacturing facilities require different layouts from blank-finishing or coating-only operations.
Controlled environments, ventilation and cleanroom requirements should be established through process-specific engineering and safety assessments. The site layout should also provide suitable access for equipment installation, maintenance, emergency response and waste handling.
5. Raw Materials and Chemicals for a Carbide Inserts Manufacturing Plant in India
Powder specification and consumable control determine grade repeatability and tool life far more than machine branding does in any carbide inserts manufacturing plant in India.
5.1 Tungsten Carbide Powder and Cobalt Binder
The main raw materials are tungsten carbide powder and a cobalt or other suitable binder, with composition determined by the target grade and application. Powder particle size, purity, carbon content, oxygen level and particle-size distribution should be specified against the selected material system and supplier data. Binder content and powder characteristics affect hardness, toughness, wear resistance and sintering behaviour. Incoming materials should be verified against approved grade specifications and certificates of analysis.
5.2 Grain Growth Inhibitors and Additional Carbides
Grain-growth inhibitors and mixed-carbide additions, including titanium, tantalum, niobium, vanadium or chromium carbides, may be used to tailor substrate properties for specific cutting applications. Their selection and concentration depend on the grade formulation, grain size, binder system and intended workpiece material. Composition should be established through material development, supplier specifications and sintering trials. Coating adhesion should be evaluated separately through validated substrate preparation, deposition controls and appropriate adhesion tests.
5.3 Consumables: Binder, Targets, Gases and Diamond Wheels
Consumables depend on the selected production and coating routes. They may include pressing lubricants, milling solvents, diamond grinding wheels, coolants, coating targets and process gases. The required materials, grades, purity levels and consumption rates should be specified by the equipment supplier and validated for the selected substrate and coating system. Target purity and grain structure drive coating adhesion directly.
5.4 Chemical Storage, Cobalt Exposure and Powder Safety
Cobalt and cemented-carbide dust require a documented occupational-hygiene assessment because exposure can pose serious health risks. The facility should use enclosed powder handling where practicable, effective local exhaust ventilation, suitable dust collection and appropriate personal protective equipment. Exposure monitoring and control limits should be established with reference to applicable Indian occupational-safety requirements and recognised industrial-hygiene guidance. Do not present an international exposure guideline as a statutory Indian limit unless the applicable Indian requirement has been verified.
6. Core Process Steps for a Carbide Inserts Manufacturing Plant in India: Powder Preparation to Sintering
The front-end flow runs from weighed powder to a densified blank through four controlled stages, each with parameters that must be locked into the equipment specification.
6.1 Powder Milling, Mixing and Spray Drying
Powder, binder metal, inhibitors and pressing lubricant are charged to an attritor or ball mill with cemented carbide media in hexane or ethanol at a ball-to-powder ratio of 5:1 to 10:1 for 4-24 hours, producing a homogeneous slurry with controlled oxygen pickup. Milling conditions and granule characteristics should be established for the selected powder formulation and equipment. Final grain structure and mechanical properties depend on several interacting factors, including starting powder characteristics, composition, milling, grain-growth inhibitors, sintering conditions, and process control.
6.2 Powder Compaction and Green Blank Forming
Pressing force, compaction pressure, die configuration and green density depend on insert geometry, powder characteristics, tooling design and the selected grade. These parameters should be established through die-design calculations, supplier recommendations, and compaction trials. Uniform green density and dimensional consistency should be verified before sintering. Complex milling geometries use CNC-controlled multiple punches or CNC hydraulic presses with controlled powder transfer; large or slender parts use cold isostatic pressing at 150-300 MPa before green machining.
6.3 Dewaxing and Vacuum Sintering
Dewaxing and sintering profiles depend on the powder formulation, binder system, furnace design, and target grade. Temperature, atmosphere, pressure, heating rate, holding time and cooling conditions should be developed and validated through supplier guidance and pilot trials. Die dimensions must account for grade-specific shrinkage, which should be confirmed through process validation and dimensional inspection. Linear shrinkage of 16-22% must be compensated in die design, and carbon potential is controlled by furnace atmosphere and powder carbon.
6.4 HIP and Sinter-HIP
Vacuum sintering densifies cemented carbide through liquid-phase sintering. Hot isostatic pressing applies gas pressure at elevated temperature to reduce residual porosity, while sinter-HIP combines sintering and pressure-assisted densification in an integrated process. The need for HIP or sinter-HIP, and the applicable pressure, temperature and cycle timing, depend on the grade, porosity requirements, furnace design and product specification.
7. Core Process Steps for a Carbide Inserts Manufacturing Plant in India: Grinding, Coating and Inspection
Finishing and verification convert a sintered blank into a saleable insert whose geometry, edge condition and coating determine documented tool life.
7.1 Precision Diamond Grinding and Edge Preparation
Grinding accuracy should be specified by insert geometry, tolerance class, datum scheme and customer requirements. Inscribed-circle diameter, thickness, flatness, rake and clearance angles must meet the selected drawing and applicable tolerance standard. Tighter tolerances may be required for particular ground inserts, but should be confirmed through the product specification and machine capability study rather than stated as a universal target. Edge preparation follows: a T-land or waterfall hone, applied by brush honing or wet blasting to a 0.02-0.08 mm edge radius, controls coating adhesion and prevents micro-chipping in interrupted cuts.
7.2 PVD Coating
PVD processes, including cathodic arc and magnetron sputtering, can deposit coatings such as TiN, TiAlN and AlCrN. Coating composition, layer architecture, thickness, substrate temperature, chamber pressure, gas flow and substrate bias depend on the equipment, substrate and target application. Surface cleaning, preparation and coating conditions should be validated for the selected insert grade and coating system. PVD is often selected where lower processing temperatures and controlled edge geometry are important.
7.3 CVD Coating
CVD processes can deposit multilayer coatings, including TiN, TiCN and aluminium oxide, on suitable carbide substrates. Deposition temperature, pressure, gas chemistry, coating thickness and layer sequence depend on the selected process and coating architecture. Medium-temperature CVD may be used for certain TiCN layers, while aluminium oxide deposition typically uses a different process window.
The equipment or coating supplier should provide a validated recipe for the intended substrate and application. CVD coatings are widely used for carbide inserts in suitable steel-turning applications, where multilayer coatings can provide wear resistance and help control crater wear. The preferred coating system depends on the workpiece material, cutting speed, feed, depth of cut and operating conditions.
7.4 Inspection, Testing and Quality Control
Quality-control limits should be defined for each grade and product drawing. Testing may include hardness, density, magnetic properties, transverse rupture strength, microstructure, geometry, coating thickness and adhesion. Use the relevant test method, including ISO 3369 for density determination and ISO 3327 for transverse rupture strength, where applicable.
Acceptance ranges should be based on the grade specification, validated process capability and customer requirements, not treated as universal values for all cemented carbide inserts. Geometry is verified on a CNC vision or coordinate measuring machine, coating thickness and adhesion by calotte grinding and Rockwell indentation, and tool life by ISO 3685 turning or ISO 8688 milling tests before a grade is released.
8. Machinery, Cleanroom and Utilities for a Carbide Inserts Manufacturing Plant in India
Machinery, controlled environments and utilities account for the majority of capital and almost all of the technical risk in a carbide inserts manufacturing plant in India.
8.1 Machinery Selection and Specification Drivers
Specify sintering equipment based on temperature uniformity, atmosphere and carbon-potential control, cycle repeatability, usable batch capacity and compatibility with the intended grades. Evaluate grinders on achievable geometry and tolerance, repeatability, changeover time, automation, wheel-management systems and demonstrated production capability.
Assess coating equipment on process compatibility, chamber capacity, coating uniformity, recipe control, uptime and service support. Establish acceptance criteria through supplier documentation, factory acceptance tests and trials using representative products. Link performance guarantees to agreed quality, yield and operating requirements rather than nameplate throughput alone.
8.2 Cleanroom, Controlled Areas and Ventilation
Environmental and ventilation requirements depend on the production model, materials, contamination risks and equipment specifications. Powder handling requires suitable containment and dust controls, while grinding may require local exhaust ventilation, coolant-mist control and management of cobalt-containing dust. Sintering and coating areas need process-specific ventilation, gas handling and temperature controls.
Cleaning and inspection areas should protect product quality and prevent contamination. Cleanroom classification, humidity limits, filtration, pressure differentials and backup power should be established during detailed engineering only where justified by process or customer requirements.
8.3 Utilities: Power, Water, Gases and Vacuum
Backup power should be designed around the electrical load schedule, process interruption risks and equipment supplier requirements. Identify which loads require uninterrupted supply, which can be safely shut down and whether full process-load backup is technically and economically justified. Furnace controls, cooling systems, vacuum systems and safety functions should be addressed in the power-failure and recovery strategy.
Utilities include argon at 99.999% for HIP and sintering, nitrogen and hydrogen for dewaxing and CVD, helium for leak testing, oil-free compressed air at 6-8 bar with a minus 40 degrees C dew point, and chilled water at 12-18 degrees C for furnace and coater cooling (Figures are indicative in nature, may vary).
8.4 Plant Layout and Material Handling
Layout follows one-way process flow: powder receiving and sealed store, milling and spray drying, pressing, dewaxing and sintering, HIP, grinding, edge preparation, coating, final inspection, packing and dispatch, with the effluent plant and utility block at the perimeter. Clean and dirty traffic never cross, and the coated-insert route from chamber to packing is segregated to prevent surface contamination. Material handling uses sealed powder containers, insert trays and magazines, and interlocked pass boxes between controlled zones.
8.5 Key Machinery
| Category | Equipment | Illustrative Scale |
|---|---|---|
| Powder preparation | Attritor mill with carbide media | 100-500 kg per batch |
| Granulation | Closed-cycle spray dryer | 50-200 kg/h granules |
| Compaction | Hydraulic die press, multi-cavity tooling | 160-400 t, 8-30 cavities |
| Sintering | Vacuum sinter furnace, graphite element | 1,380-1,480 degrees C, 100-500 kg load |
| Pore closure | Sinter-HIP or HIP furnace | 1,000-1,500 bar argon |
| Grinding | 5-axis CNC insert grinder | 20-40 inserts per hour |
| Edge preparation | Brush honing and wet blast unit | 0.02-0.08 mm edge radius |
| Coating | Cathodic arc PVD or CVD reactor | 200-600 inserts per PVD run |
9. Effluent, Licences and Project Economics for a Carbide Inserts Manufacturing Plant in India
Effluent, residues and approvals determine whether an otherwise sound carbide inserts manufacturing plant in India is ever allowed to run at design capacity.
9.1 Effluent, Grinding Sludge and Water Treatment
Wastewater may arise from grinding coolants, equipment cleaning, wet blasting and coating pretreatment, depending on the production route. Treatment should be designed after characterising the actual waste streams and may include solids separation, filtration, pH adjustment and additional treatment where required. Effluent quality must meet the applicable regulatory standards and State Pollution Control Board consent conditions. Zero-liquid-discharge systems should be incorporated where required by the applicable permissions or project design basis.
9.2 Air Emissions, Dust and Hazardous Waste
Potential emissions and waste streams depend on the process route and materials used. Dewaxing, sintering, grinding, and coating may require different ventilation, dust collection, or exhaust-treatment systems based on the identified contaminants and applicable requirements. Grinding sludge, spent coolant, used oils, filter media, and coating residues should be characterised and classified under the applicable waste rules. Storage, authorisation, recordkeeping, transport, and disposal arrangements should follow the relevant regulatory requirements and site permissions.
9.3 Licences, Registrations and Approvals
The approvals required depend on the production route, site, installed equipment, gas-storage arrangements and waste streams. They may include:
- Environmental consents: Consent to Establish (CTE) before establishing the unit and Consent to Operate (CTO) before commencing operations, from the relevant State Pollution Control Board (SPCB) or Pollution Control Committee (PCC), as applicable.
- Waste authorisation: Authorisation under the Hazardous and Other Wastes (Management and Transboundary Movement) Rules, 2016, where applicable to the waste generated or handled. Grinding sludge, spent coolant, used oils and other residues should be characterised before classification.
- Factory and building approvals: Applicable factory registration or licensing, building-plan approval, fire-safety permissions and occupational-safety compliance under the Occupational Safety, Health and Working Conditions Code, 2020, and applicable rules and notifications.
- Gas-storage approvals: Assess requirements under the applicable PESO-administered rules based on gas type, quantities, cylinders or vessels, and storage configuration. Do not assume that every installation requires the same licence.
- Other approvals: Boiler registration, groundwater permissions and electrical-safety approvals where applicable.
Environmental Clearance under the EIA Notification, 2006 should be assessed against the specific project configuration and applicable amendments. Confirm the approval list with the relevant authorities before finalising the project design.
9.4 CAPEX and OPEX Composition
CAPEX and OPEX should be estimated from a defined production model, equipment list, process route, site and utility requirements, supplier quotations and working-capital assumptions. Cost shares vary significantly between coating-only, blank-finishing and integrated powder-to-insert facilities. Any percentage breakdown should be reconciled to a clearly defined total and should state whether land, contingency, installation, taxes, financing costs and working capital are included.
9.5 Project Economics
The investment required for a carbide inserts manufacturing plant depends on the production model, capacity, machinery, level of integration, site infrastructure and working-capital requirements. A coating-only facility, a grinding and finishing plant, and a fully integrated powder-to-insert operation have different cost structures. A reliable estimate should be developed using a defined project scope, supplier quotations, and project-specific cost assumptions.
Conclusion
A carbide inserts manufacturing project requires coordinated planning across material selection, powder metallurgy, grinding, coating, inspection and occupational safety. Machinery selection alone does not establish commercial viability. Investors must also validate product specifications, process capability, supplier support, qualification requirements, environmental controls, and production costs. A project-specific feasibility study and detailed engineering assessment can help align the production model with the intended market and investment objectives.
Three priorities should guide project development. First, choose between integrated manufacturing, blank finishing, and coating-only operations before finalising capacity and investment. Second, size equipment around the planned product mix, validated cycle times, and achievable saleable output. Third, address environmental permissions, occupational-safety controls, gas-storage requirements, and customer qualification alongside engineering and procurement.
IMARC Engineering supports manufacturing projects through feasibility assessment, equipment selection, plant layout, utilities planning, regulatory approvals, and commissioning support. These services can help investors evaluate technical requirements and develop a project plan based on defined production and investment assumptions.
PURSUING A CARBIDE INSERTS MANUFACTURING PLANT IN INDIA?
IMARC Engineering supports investors, project sponsors and manufacturers with capacity and feasibility planning, site selection, plant layout, equipment selection, utility and gas system design, cobalt containment and ventilation engineering, effluent treatment planning, regulatory approvals and capital investment planning. The advisory covers solid and indexable carbide inserts, turning and milling grades and coated tooling, including powder preparation, compaction, vacuum sintering and sinter-HIP, diamond grinding, PVD and CVD coating and final inspection, with project-specific infrastructure and commissioning planning.
→ Schedule a free carbide inserts scoping consultation with an IMARC specialist
Frequently Asked Questions
Decide the production model first: full powder-to-insert, purchased-blank finishing, or coating-only. Prepare a DPR covering grade portfolio, grinding hours, machinery, layout, utilities and cost; secure industrial land and State Pollution Control Board Consent to Establish; then commission sintering, grinding and coating in sequence. Qualify each grade against ISO 3685 or ISO 8688 tool-life tests before commercial dispatch.
Integrated manufacturing generally involves powder preparation, milling, granulation, compaction, dewaxing and sintering, followed by precision grinding, edge preparation, coating and inspection. The exact process depends on the selected grade, insert geometry and coating system. Operating parameters should be validated through supplier specifications, process trials and product-quality testing.
Equipment may include powder mills, spray dryers, hydraulic presses, vacuum sintering furnaces, HIP systems where required, CNC diamond grinders, edge-preparation units, PVD or CVD coating systems, cleaning equipment and inspection instruments. The final machinery list depends on the production model, grade portfolio, target capacity and quality requirements.
Investment depends on production capacity, manufacturing route, machinery, automation, site infrastructure, utilities, environmental controls and working capital. Coating-only facilities, blank-finishing plants and integrated powder-to-insert operations have different cost structures. A reliable estimate requires a defined project scope, supplier quotations and project-specific engineering and financial assessments.
The principal materials are tungsten carbide powder and a metallic binder, commonly cobalt. Some grades also use grain-growth inhibitors or additional carbides to achieve specific hardness, toughness and wear-resistance characteristics. Material specifications and proportions depend on the intended cutting application, grade formulation and validated manufacturing process.
Sintering densifies a compacted carbide component through controlled heating, while hot isostatic pressing (HIP) applies gas pressure at elevated temperature to reduce residual porosity. Sinter-HIP combines sintering and pressure-assisted densification in an integrated process. The appropriate route depends on grade requirements, porosity limits, equipment capabilities, and product specifications.
Requirements depend on the production route and equipment selected. Facilities may need controlled powder handling, dust collection, local exhaust ventilation, grinding-coolant management, electricity, cooling water, compressed air, vacuum systems and process gases. Cleanroom classification, humidity controls, backup power and gas-storage arrangements should be established through detailed engineering and risk assessment.
Depending on the project, approvals may include SPCB Consent to Establish and Consent to Operate, factory registration or licensing, building and fire approvals, and hazardous-waste authorisation where applicable. PESO requirements for gas storage, boiler registration, groundwater permissions and electrical-safety approvals should be assessed separately. Environmental Clearance applicability requires project-specific verification.
Yes. A manufacturer can start by purchasing sintered carbide blanks and investing in grinding, edge preparation, coating, and inspection. This reduces the need for in-house powder preparation and sintering equipment but creates dependence on blank suppliers. Grinding may still generate cobalt-containing dust, so suitable containment, local exhaust ventilation, dust collection and occupational-exposure controls remain necessary. Investment requirements should be established through a project-specific cost model.
They build the grade and capacity model around grinding hours, test full-integration against blank-finishing on life-cycle cost, specify presses, sinter furnaces, grinders and coaters with acceptance criteria, design layout, controlled areas, cobalt containment and gas systems, sequence SPCB, hazardous-waste, factory and PESO approvals, structure CAPEX and OPEX, and manage procurement, construction, installation and commissioning under EPCM delivery.
Recent Post
Trusted by Industry Leaders
We partner with global enterprises and ambitious businesses across sectors to deliver operational excellence, strategic insights, and sustainable growth through integrated solutions.
Success in Their Words
Real feedback from clients across industries. Discover how our solutions delivered measurable impact and operational excellence.
I wanted to express my sincere appreciation for your efforts in handling this matter. Your dedication and commitment have been truly commendable, and it is evident that you have put in tremendous hard work and expertise into resolving the issues at hand. We are greatly interested in continuing our collaboration with you in the future, as your professionalism and reliability have made you a trusted partner. Thank you once again for your invaluable contribution. We look forward to strengthening our partnership ahead.
It has been a pleasure working with the IMARC team. The insights provided were structured, clear, and highly valuable, helping us strengthen both our technical and financial planning with confidence. We deeply appreciate the team’s professionalism, responsiveness, and attention to detail throughout the engagement. Every requirement was well understood and effectively incorporated, resulting in a comprehensive and actionable output. Overall, our experience has been excellent, and I would gladly recommend IMARC to organizations seeking a reliable research partner.
Your service is truly exceptional. Working with the IMARC team has been a seamless and professional experience. The clarity of communication, responsiveness to queries, and consistent support at every stage made the entire engagement highly efficient. The insights shared were well-structured, practical, and perfectly aligned with our requirements, helping us make informed decisions with confidence. Overall, the dedication and professionalism demonstrated by your team stand out, and I would be glad to recommend IMARC as a reliable and trustworthy research partner.
IMARC did an outstanding job in preparing our study. They were punctual, precise, and consistently responsive throughout the entire process. The team delivered all the data we required in a clear, well-organized, and highly professional format. Their strong attention to detail, combined with their ability to meet every deadline without compromising quality, truly set them apart. Overall, their reliability and commitment made them an exceptional partner for our project, and we would gladly work with them again in the future.
IMARC made the whole process incredibly easy from start to finish. Everyone I interacted with via email was polite, professional, and straightforward to deal with, always keeping their promises regarding delivery timelines and remaining consistently solutions-focused. From my very first contact, I appreciated the professionalism and support shown by the entire IMARC team. I highly recommend IMARC to anyone seeking timely, affordable, and reliable information or advice. My experience with IMARC was excellent, and I truly cannot fault any aspect of it.
I’d like to express my sincere gratitude for the excellent work you accomplished with the study. Your ability to quickly understand our requirements and deliver high-quality results under tight timelines truly reflects your expertise, exceptional work ethic, and unwavering commitment to your customer’s success. The professionalism and responsiveness you demonstrated throughout the process made a significant difference. Our entire team and company are incredibly thankful for your dedication, reliability, and support. Once again, thank you for your outstanding contribution.